

Heat Treatment
now browsing by tag
Pre-Hardened vs. Annealed Die Blocks: Which Saves More Machining Time
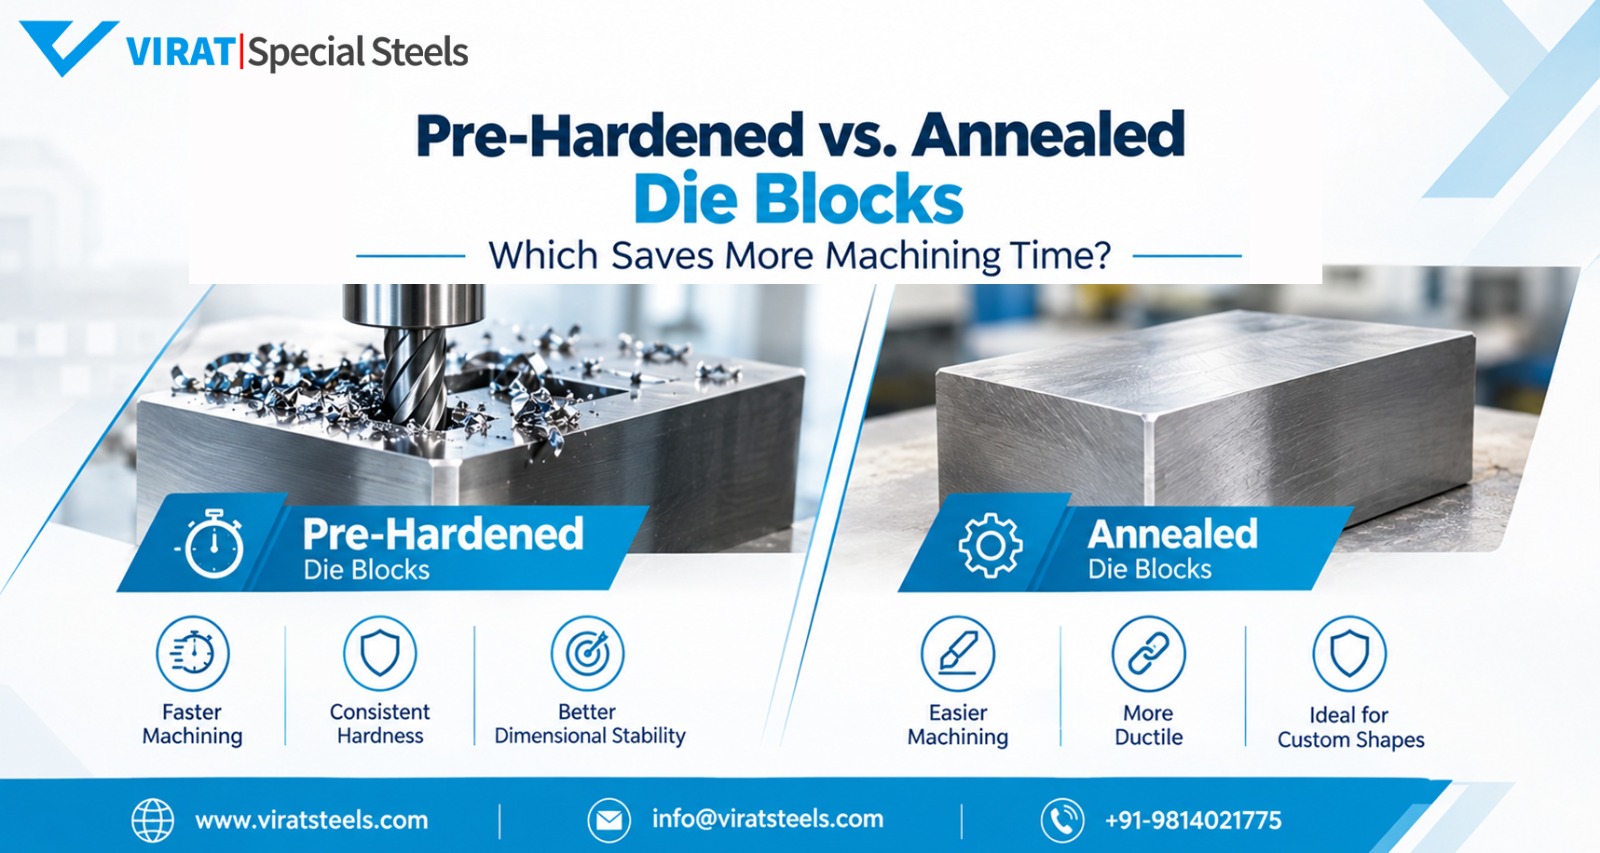
Ask three machinists whether Pre-Hardened vs. Annealed Die Blocks save more machining time, and you will probably hear three different answers. Each one can be right, because each is measuring something different.
If you count the hours the cutter spends in the steel annealed wins. The steel is softer so you can push harder. But a die block is not finished when roughing ends. It still has to go out for hardening, come back, be ground or EDM’d to size, and sometimes be corrected because it moved. Count all of that, and a pre-hardened block such as P20 or P20+Ni often reaches a finished tool sooner.
We have been supplying tool and die steels since 1957, and this is one of the oldest debates in any toolroom. Here is how we would think it through, using the hardness figures from our own product pages.
Pre-Hardened vs Annealed Die Blocks in One Minute
Annealed die blocks arrive soft. They cut quickly and go easy on tools, but they must be hardened and tempered after machining. H13 and D2 are the usual examples.
Pre-hardened die blocks arrive already hardened and tempered. They cut more slowly and need better tooling, but once machined, you are done: no furnace, no waiting. P20 and P20+Ni are the usual examples.
Heavy material removal or a high working hardness? Look at annealed. Moderate removal, tight tolerances and a deadline? Pre-hardened is usually the safer bet.
What Are Annealed Die Blocks?
Annealed die blocks are softened at the mill so they machine easily. On our datasheets, H13 is soft annealed to a maximum of 240 HB and HCHCR-D2 to a maximum of 250 HB. That is soft enough for fast roughing, drilling and tapping.
The catch is that annealed steel is not ready to work. After machining, it has to be hardened and tempered. H13 is hardened at roughly 1030 to 1060 °C and then tempered back to a working hardness, typically 44 to 52 HRC. D2 can be taken to 55 to 62 HRC. Then comes finishing.
What you gain: quick roughing, long tool life, and a working hardness that pre-hardened steel simply cannot reach.
What it costs you: an extra process (usually an outside heat treater), size change during hardening, and a small but real risk of distortion or cracking.
What Are Pre-Hardened Die Blocks?
Pre-hardened die blocks are hardened and tempered at the mill before they reach you. P20 is supplied at roughly 28 to 34 HRC, and P20+Ni at around 280 to 320 HB, with the nickel keeping hardness more even through thick sections. For tougher duty, there is a higher-hardness P20+Ni variant, HXM 24, at 360 to 400 BHN.
You machine the block to final dimensions and it goes into service. The hardness is fixed, so you cannot raise it, and these grades are not the right choice for very abrasive duty. Nitriding or flame hardening can add a tougher outer layer to the cavity face.
What you gain: no heat treatment, no hardening distortion and a shorter route to a mould.
What it costs you: faster tool wear while cutting, and a ceiling on how hard the finished tool can be.
Why Annealed Die Blocks Save Machining Time
On the machine softness feels like a gift. Lower cutting forces mean you can run feeds and take deeper cuts. The tools stay cooler and last longer so the operator changes inserts often. Drilling cooling channels or tapping ejector holes, which can be miserable in harder steel, becomes routine work.
It matters most on big blocks with a lot of steel to remove.If you are carving out a cavity or if you are carving out a large die profile, a small saving, on every cubic centimetre adds up to many hours. Many shops rough in the soft state, stress relieve, then harden and finish. For D2, our datasheet calls for stress relief after rough machining at roughly 600 to 650 °C.
The Machining Time Paradox: Material Removal Volume
Here is the paradox: annealed steel is faster to cut, but it is not always faster to finish. What decides it is how much steel you remove compared with the largely fixed time that heat treatment takes.
The penalty for cutting harder steel grows with volume. Remove a little and you barely notice; remove a lot and it hurts. Heat treatment is different. Hardening, tempering, transport, the wait for a furnace slot and the finishing afterwards take about the same time whether your cavity is shallow or deep.
Think of it as a break-even point. A shallow-cavity mould usually finishes faster in pre-hardened steel. A deep, heavily profiled die often finishes faster in annealed steel. We cannot give you one percentage that works for every shop, because it depends on your machine, your tooling and your heat treater. The best way to find out is to run a trial cut and track your cycle times.
When Pre-Hardened Blocks Save Time Instead
Pre-hardened wins when you count the whole job, not just the spindle.
No Heat Treatment in Your Schedule
Without hardening, the block does not go to a heat treater, so you do not wait for a furnace slot or for the block to come back. On prototype tools and urgent mould work, that gap alone can outweigh the extra cutting time. Research from Chalmers University on mould steels makes the same point: the pre-hardened condition has become popular because of its shorter lead times compared with roughing soft and hardening later.
Even Hardness Through Thick Blocks
On a mold base if the hardness is not even the cutting tool will act differently from the outside to the inside. This is why we usually suggest to people buying blocks to go with P20+Ni. The nickel, in this material helps make the hardness even all the way through.
Less Distortion, Less Rework
The block is already at working hardness, so there is no hardening distortion to chase afterwards. You can leave smaller finishing allowances and skip much of the grinding and EDM correction. Heavy machining can still leave behind stress in the metal. That’s why our P20 datasheet says to stabilize machined dies at about 460 to 500 °C just before doing the final machining.
Getting the Most Out of Pre-Hardened Steel
Use machines and holders use coated carbide tooling and use the cutting data from your tool supplier. Keep cuts consistent. Clear the chips well. Do not run parameters on it and hope for the best.
Machining Time: Pre-Hardened vs Annealed Die Blocks
Here is how the two compare side by side, using the grades we stock.
| Factor | Annealed (H13, D2) | Pre-Hardened (P20, P20+Ni) |
| Supplied hardness | H13 max 240 HB, D2 max 250 HB | P20 about 28 to 34 HRC, P20+Ni about 280 to 320 HB |
| Cutting speed and feed | Higher | Lower |
| Tool wear | Lower | Higher; carbide preferred |
| Roughing time on large removal | Shorter | Longer |
| Heat treatment after machining | Required | Usually not required |
| Distortion risk | During hardening | Low; only stress release |
| Overall lead time | Longer, includes heat treatment | Often shorter |
| Working hardness | H13 about 44 to 52 HRC, D2 55 to 62 HRC after treatment | Fixed at supplied hardness; surface can be nitrided |
| Typical use | Die casting, forging, extrusion, stamping dies | Injection moulds, mould bases, bolsters |
Figures are from the Virat Special Steels product pages. Confirm them against the mill test certificate for your lot.
What to Check Before You Order
Two blocks that have the same grade name can behave differently so don’t just look at the label. Check the hardness that is provided and how even it is, throughout the section. Look at the thickness. The shape you need. The shape you need could be flat, square or round. Also check the paperwork. If you are purchasing H13 for aluminum die casting ask about the ESR grade well.
Chemical composition, hardness range and standards are different for each grade and each supplier. Trust the datasheet and certificate, for the material you actually get.
Where Each Type Is Used Pre-Hardened vs Annealed Die Blocks
Annealed Die Blocks
Annealed grades go into tools that need high working hardness. H13 is commonly used for aluminium and zinc die casting, as well as for hot forging and extrusion dies. DB6 (DIN 1.2714) is often chosen for forging and hammer forging dies, where toughness under shock is more important than hot hardness. D2 is well suited to blanking, punching and stamping dies, as well as shear blades and slitters.
Pre-Hardened Die Blocks
Pre-hardened grades fit tools where machinability and speed matter more than extreme hardness. P20 and P20+Ni are used in injection mould cavities, cores, mould bases, bolsters, die holders and press cassettes for consumer goods and domestic appliance tooling and P20 tooling is common, in these applications. .
How to Choose Between Pre-Hardened vs. Annealed Die Blocks
If you are stuck, run through these questions:
- What hardness does the finished tool need? Above the pre-hardened range, annealed is your answer.
- How long will the tool run, and how abrasive is the material going through it?
- How much steel are you actually removing?
- How tight are the tolerances, and how complex is the shape?
- How soon do you need it?
- Do you have a heat treater you trust nearby?
Still not sure what to do? Send us the drawing and the length of the run you are expecting. We will help you figure it out.
Why Choose Virat Steels Pre-Hardened and Annealed Die Blocks
We started in 1957 as Dhingra Mill Store. Virat Special Steels now carries around 3,500 tons of stock across 35+ grades, in two yards: Ludhiana (Punjab) and Gurgaon (Haryana). That is why many orders can go straight off the shelf. For die blocks, it also means you can get both sides of this article from one supplier.
- Pre-Hardened vs. Annealed Die Blocksunder one roof.Hot work and cold work grades like H13, DB6 and D2, and plastic mould steels like P20 and P20+Ni.
- Mill-backed material. We stock steels from mills such as Swiss Steel Group, NLMK Verona, Lucchini RS and ThyssenKrupp.
- Technical help, not just a price. Our team advises on material choice, heat treatment and machining, so you pick the condition that saves you time.
- Paperwork you can show your customer. Mill test certificates and quality assurance reports come with every order, and our ISO and MSME certificates are on our downloads page.
- Quick quoting.Use the enquiry form, call +91-98140 21775, or message us on WhatsApp.
Questions Buyers Ask Before Ordering Die Blocks
Is P20 pre-hardened, or do I have to harden it after machining?
P20 is supplied pre-hardened at roughly 28 to 34 HRC, so you can machine it and put it into service right away. No hardening step is needed. If you want a tougher surface on the cavity, you can add it by nitriding.
Should I buy H13 annealed or pre-hardened for die casting?
H13 is normally supplied annealed. You machine it, harden and temper it, then finish. For specific applications we can supply pre-hardened H13, and our product page quotes 460 to 500 BHN. Tell us the application first.
Will pre-hardened steel really save me machining time over annealed?
It saves total time because you skip heat treatment, but the cutter works harder. If you are removing a lot of steel, annealed can be quicker at the machine. Look at the whole job, not just the cutting.
What is the difference between P20 and P20+Ni?
P20+Ni has added nickel. Nickel gives uniform hardness through thick sections. Nickel also gives a polish. It is the usual pick for big mould blocks and mirror finishes. P20 is the economical choice for small to medium blocks.
How thick can I get P20?
Our P20 page lists sections up to 255 mm thick. For larger blocks, talk to us. P20+Ni is often the better fit for large sections.
What hardness will I get if I harden H13 or D2 myself?
On our datasheets, H13 reaches about 55 HRC as quenched and D2 about 63 HRC. Both are then tempered, typically to 44 to 52 HRC for H13 and 55 to 62 HRC for D2. Your heat treater sets the exact cycle.
Can I machine pre-hardened steel with normal tooling?
You can, but carbide tooling and a rigid setup make life much easier. Reduce your speeds and feeds compared with annealed steel, and follow your tool maker’s advice.
Do I need to stress relieve a pre-hardened block?
For heavily machined dies, stabilise the block at roughly 460 to 500 °C just before finish machining, then air cool. Our P20 datasheet advises this, and it is cheap insurance on a big mould.
Can P20 or P20+Ni be nitrided?
Yes. Both respond well to nitriding, and P20+Ni can also be flame hardened to create a harder surface. Check the nitriding temperature with your heat treater so that the block does not become soft. .
Can pre-hardened steel be welded for mould repair?
Yes, with a matching filler and the right procedure. For P20, our page suggests a preheat of 200 to 300 °C and post-weld tempering. Ask us before you start on a critical repair.
H13 or DB6 for my forging die?
DB6, DIN 1.2714 standard is the preferred metal when you need a piece that can take a hard hit. DB6 works best for forging and hammer forging because toughness under shock matters most. H13 is the choice, for die casting and extrusion because heat resistance and thermal fatigue matter most.
Do you supply ESR H13?
Yes. ESR H13 is suggested for aluminum pressure die casting and other situations that involve temperature and high pressure. Let us know about your use and we will give you guidance.
Do you send test certificates with the steel?
Yes. We offer mill test certificates and quality assurance reports with each order. If your project requires anything let us know as soon, as possible.
Which sizes and shapes do you supply?
Flat bars, square bars and round bars, in the sizes that fit your requirement. Just let us know the dimensions and quantity that you need.
Where do you ship from, and how fast can you deliver?
We have stock, in Ludhiana and Gurgaon and I supply across India. Delivery time depends on grade, size and your location so give me the details and I will confirm .
How do I get a quote?
Send the grade, condition, size and quantity through our enquiry page, email info@viratsteels.com, or call +91-98140 21775.
So, Which Saves More Machining Time?
If you are counting spindle hours, annealed die blocks win, especially when there is a lot of steel to remove or you need a high final hardness. If you are counting days to a finished tool, Pre-Hardened vs. Annealed Die Blocks often win, because they skip heat treatment and avoid hardening distortion.
Not sure which suits your next job? Talk to the Virat Steels team. Send us the grade, size, condition and quantity through our enquiry page, call +91-98140 21775, or email info@viratsteels.com. We will help you compare Pre-Hardened vs. Annealed Die Blocks options and put a quote together.
DB6 Tool Steel Hardness (HRC): Complete Guide to Heat Treatment & Applications
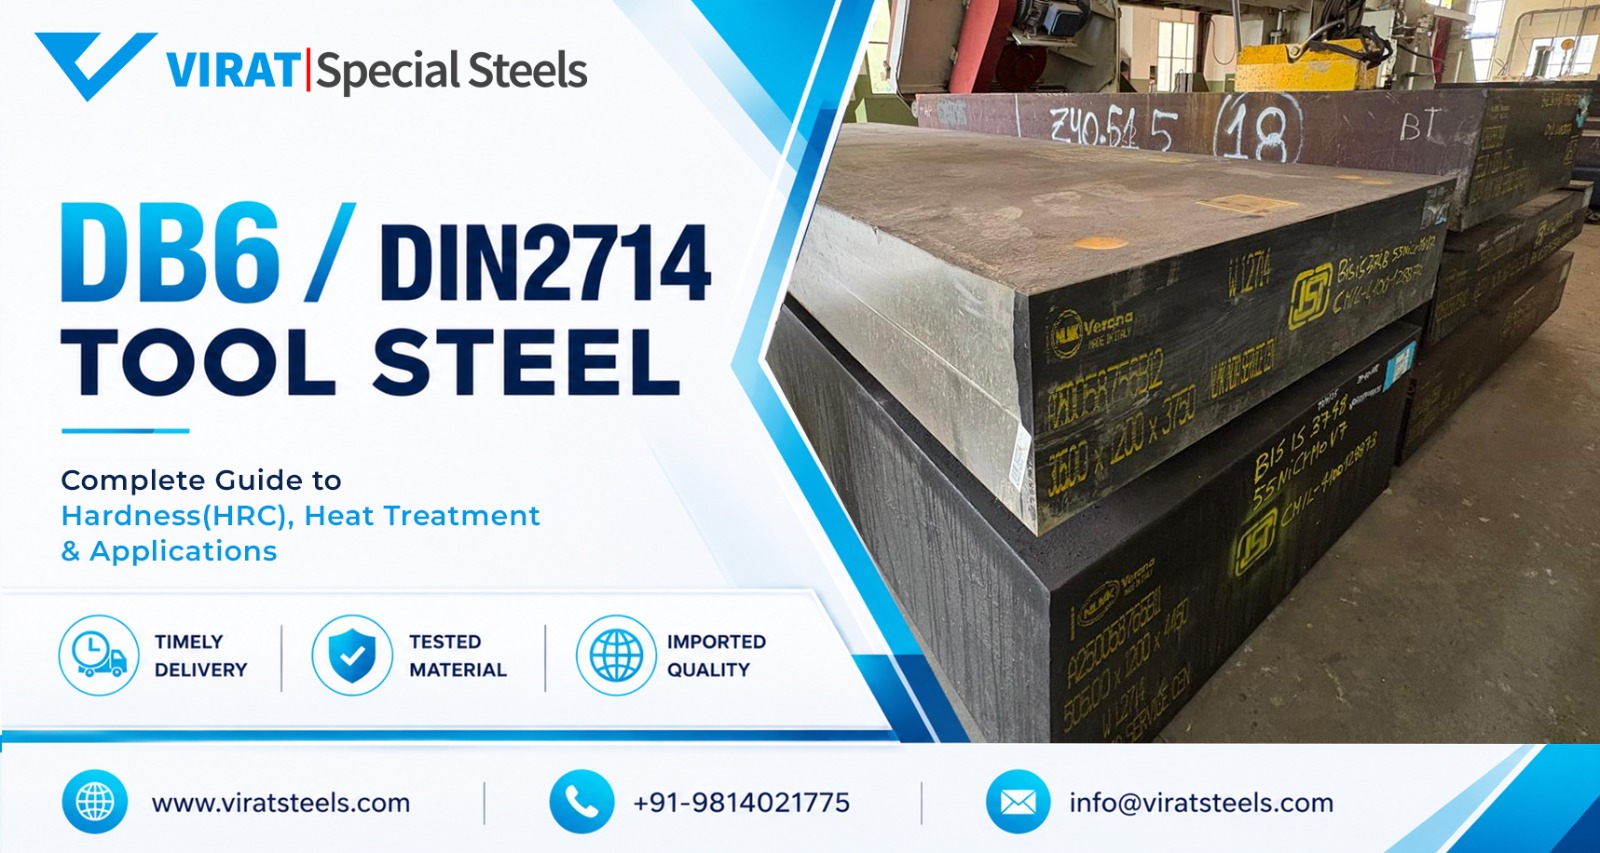
DB6 Material Hardness in HRC
DB6 Tool Steel (DIN 1.2714) is a widely used hot work tool steel for forging, die casting, heavy engineering and plastic mould industries. It offers an excellent balance of toughness, wear resistance, impact strength, and heat resistance, making it suitable for demanding industrial applications.
Hardness of DB6 Tool Steel is an important factor that defines its performance properties, tool life, machinability and ability to resist deformation under high pressure and high temperature conditions. The right heat treatment to the correct Rockwell Hardness (HRC) will ensure optimum performance in forging dies, extrusion dies, hammer dies and pressure die casting application.
In this comprehensive guide, we cover DB6 Tool Steel hardness (HRC), heat treatment process, mechanical properties, applications, comparison with other tool steels, pricing considerations, and why Virat Steels is one of India’s trusted suppliers of premium-quality DB6 Tool Steel.
What is DB6 Steel?
DB6 Tool Steel is a high quality hot work tool steel, equivalent to DIN 1.2714, (AISI L6), (55NiCrMoV7). It is a nickel-chromium-molybdenum-vanadium alloy steel known for outstanding toughness and excellent resistance to thermal fatigue.
Compared to conventional hot work steels, DB6 provides:
- Superior impact strength
- High toughness
- Excellent wear resistance
- Good hardenability
- Outstanding resistance to cracking
- Longer die life
- Excellent polishability
- Good machinability
These characteristics make DB6 an ideal choice for large forging dies, hammer dies, die holders, extrusion tooling, pressure die casting dies, and heavy-duty industrial tools.
International Equivalents of DB6 Tool Steel
DB6 Tool Steel is internationally recognized under the DIN 1.2714 standard and is equivalent to EN 55NiCrMoV7. It is also considered an approximate equivalent to AISI L6 in certain applications. In India, DB6 is widely known by its trade name and is commonly used as a premium hot work tool steel for forging dies, die casting dies, extrusion tooling, and heavy engineering applications.
Chemical Composition of DB6 Tool Steel
DB6 Tool Steel contains a balanced combination of carbon, chromium, nickel, molybdenum, and vanadium, providing excellent toughness, wear resistance, and hot strength. This alloy composition ensures superior impact resistance, good hardenability, and extended tool life in demanding hot work applications.
| Element | Composition (%) |
| Carbon (C) | 0.50–0.60 |
| Silicon (Si) | 0.10–0.40 |
| Manganese (Mn) | 0.65–0.95 |
| Chromium (Cr) | 1.00–1.20 |
| Nickel (Ni) | 1.50–1.80 |
| Molybdenum (Mo) | 0.45–0.55 |
| Vanadium (V) | 0.07–0.12 |
Mechanical Properties of DB6 Tool Steel
DB6 Tool Steel offers an excellent combination of toughness, wear resistance, and heat resistance, making it ideal for high-impact and hot work applications such as forging and die casting.
| Property | Typical Value |
| Density | 7.85 g/cm³ |
| Tensile Strength | High |
| Toughness | Excellent |
| Wear Resistance | Excellent |
| Heat Resistance | Excellent |
| Thermal Fatigue Resistance | Excellent |
DB6 Tool Steel Hardness (HRC)
Hardness is the most important property when selecting DB6 Tool Steel for industrial tooling.
Different hardness according to different Tempering temperature conditions.
– Annealed condition – 255 BHN max
– Hardened and Tempered condition- 38 to 42 HRC
annealed stock measures up to 255 BHN, standard mill-supply condition is tempered to 38–42 HRC for machining, and finished dies are re-hardened and tempered to a working hardness of 45–56 HRC depending on whether the application prioritizes toughness or wear resistance.
Heat Treatment of DB6 Tool Steel
Proper heat treatment is essential to achieve the desired hardness and mechanical properties.
The process generally involves:
- Annealing
- Stress Relieving
- Hardening
- Quenching
- Tempering
Each stage contributes to the final balance of hardness, toughness, and dimensional stability.
Annealing
Annealing softens the material, improves machinability, and relieves internal stresses before hardening.
Recommended Process:
- Heat slowly to 840–860°C
- Hold for sufficient soaking time
- Cool slowly inside the furnace
Resulting Hardness:
Approximately 220–250 HB
Stress Relieving
Stress relieving is recommended after rough machining.
- Temperature: 600–650°C
- Hold for 2 hours
- Furnace cool slowly
This minimizes distortion during final hardening.
Hardening
The hardening process significantly increases hardness and wear resistance.
Procedure:
- Preheat: 600 – 650°C
- Austenitize: 840–870°C
- Oil or polymer quench
- Air cooling where appropriate
The resulting hardness typically reaches 54–56 HRC before tempering.
Tempering
Tempering reduces brittleness while maintaining the desired hardness.
It is recommended to temper immediately after quenching.
Typical Tempering Range:
450–650°C
Double tempering is often recommended for improved dimensional stability and toughness.
Advantages of Proper Heat Treatment
By improving the mechanical properties and durability of the steel, proper heat treatment can improve the performance and service life of DB6 Tool Steel.
- Enhanced wear resistance
- Greater durability
- Improved thermal fatigue resistance
- Less risk of cracking
- Longer life of die
- Reduced maintenance costs
Applications of DB6 Tool Steel
DB6 Tool Steel (DIN 1.2714) is a popular choice for hot work applications requiring high toughness, wear resistance and resistance to thermal fatigue. It is ideal for the manufacture of heavy duty dies and tools used under extreme operating conditions.
| Industry | Typical Applications |
| Forging | Closed forging dies, hammer dies |
| Die Casting | Aluminium die casting dies |
| Extrusion | Extrusion dies |
| Automotive | Crankshaft and connecting rod dies |
| Plastic Moulding | Large mould bases |
| Heavy Engineering | Die holders and forging blocks |
| Aerospace & Defence | Heavy-duty tooling |
| Steel Plants | Hot shearing blades and press tools |
DB6 Tool Steel Advantages & Disadvantages
| Advantages | Disadvantages |
| Good impact resistance and toughness | More expensive than the usual alloy steels |
| Good wear and heat fatigue resistance | Needs proper heat treatment |
| Longer die life with less cracking | Not the best choice for high abrasive cold work applications (D2 is preferred) |
| Good hardenability and dimensional stability | Special tools are required for machining after hardening |
| Suitable for large forging dies, hot working tools | Material costs are higher for more expensive alloys |
DB6 vs H13 Tool Steel Comparison
| Property | DB6 Tool Steel (DIN 1.2714) | H13 Tool Steel (DIN 1.2344) |
| Steel Type | Hot Work Tool Steel | Hot Work Tool Steel |
| Toughness | Excellent | Very Good |
| Wear Resistance | Very Good | Excellent |
| Impact Resistance | Excellent | Very Good |
| Thermal Fatigue Resistance | Excellent | Excellent |
| Hot Hardness | Very Good | Excellent |
| Best Applications | Forging Dies, Hammer Dies | Die Casting & Extrusion Dies |
| Large Die Blocks | Excellent | Very Good |
| Relative Cost | Moderate | Moderate to High |
Best Choice: Choose DB6 for heavy-impact forging applications requiring superior toughness, while H13 is ideal for high-temperature die casting and aluminium extrusion tooling.
DB6 vs H11 Tool Steel
| Property | DB6 | H11 |
| Toughness | Excellent | Excellent |
| Wear Resistance | Higher | Good |
| Hardness | 45–56 HRC | 44–52 HRC |
| Thermal Shock | Excellent | Excellent |
| Large Blocks | Excellent | Good |
| Service Life | Longer | Good |
Best Choice: DB6 is preferred where higher wear resistance and longer tool life are required.
DB6 vs D2 Tool Steel
| Property | DB6 | D2 |
| Type | Hot Work | Cold Work |
| Toughness | Excellent | Moderate |
| Wear Resistance | High | Very High |
| Hot Strength | Excellent | Poor |
| Impact Resistance | Excellent | Moderate |
| Forging Dies | Excellent | Not Recommended |
| Cold Blanking | Not Ideal | Excellent |
Best Choice: Use DB6 for hot work and D2 for cold work applications.
DB6 vs P20 Tool Steel
| Property | DB6 | P20 |
| Toughness | Excellent | Good |
| Hardness | Up to 56 HRC | 28–34 HRC |
| Plastic Moulds | Good | Excellent |
| Forging | Excellent | Not Recommended |
| Wear Resistance | High | Moderate |
| Tool Life | Longer | Moderate |
DB6 vs EN31
| Property | DB6 | EN31 |
| Steel Type | Hot Work Tool Steel | High Carbon Steel |
| Toughness | Excellent | Moderate |
| Hardness | 56 HRC | 60–64 HRC |
| Impact Resistance | Excellent | Low |
| Hot Applications | Excellent | Poor |
| Bearings | Not Suitable | Excellent |
DB6 Tool Steel vs Other Tool Steel Grades
| Steel Grade | Toughness | Wear Resistance | Heat Resistance | Typical Hardness | Ideal Applications |
| DB6 (DIN 1.2714) | Excellent | Very Good | Excellent | 45–56 HRC | Forging Dies , Hammer Dies |
| H13 (DIN 1.2344) | Very Good | Excellent | Excellent | 44–54 HRC | Die Casting, Extrusion Dies |
| H11 (DIN 1.2343) | Excellent | Good | Very Good | 44–52 HRC | Hot Work & Extrusion Tooling |
| D2 (DIN 1.2379) | Good | Excellent | Moderate | 58–62 HRC | Cold Work Dies, Punches |
| P20 (DIN 1.2311) | Good | Moderate | Moderate | 28–34 HRC | Plastic Injection Moulds |
| EN31 | Moderate | Excellent | Low | 60–64 HRC | Bearings, Rollers & Wear Parts |
“DB6 Tool Steel Equivalents Explained: SKT4, 55NiCrMoV7, L6 & DIN 1.2714 Compared”
| Property | DB6 | SKT4 | 55NiCrMoV7 | L6 | DIN 1.2714 |
| Standard | Commercial | JIS | EN | AISI | DIN |
| Steel Type | Hot Work | Hot Work | Hot Work | Low Alloy | Hot Work |
| Toughness | Excellent | Excellent | Excellent | Excellent | Excellent |
| Wear Resistance | Excellent | Very Good | Excellent | Good | Excellent |
| Hardness | 45–56 HRC | 45–54 HRC | 45–56 HRC | 45–55 HRC | 45–56 HRC |
| Hot Work Performance | Excellent | Very Good | Excellent | Moderate | Excellent |
| Main Difference | Trade Name | JIS Grade | EN Grade | Approx. Equivalent | DIN Grade |
DB6, DIN 1.2714, and 55NiCrMoV7 are essentially the same steel grade with different designations. SKT4 is a close Japanese equivalent, while AISI L6 is an approximate equivalent with similar toughness but comparatively lower hot-work performance.
Available Sizes of DB6 Tool Steel
Virat Special Steels supplies DB6 Tool Steel in a wide range of standard and custom sizes to meet the requirements of die makers, tool rooms, automotive, engineering, and precision manufacturing industries.
Available Sizes (Flat)
- Thickness: 13 mm – 1500 mm
- Width: 13 mm – 3000 mm
- Length: Available in standard mill lengths or custom-cut sizes on request.
Available Sizes (Round)
- Diameter: 13 mm – 1500 mm
- Length: Standard mill lengths and customized cut-to-size options available.
Custom Processing Services
To minimize machining time and material wastage, we also offer:
- Precision cut-to-size material
- Bandsaw cutting
- Surface machining (on request)
- Bulk supply with batch-wise traceability
- Material Test Certificate (MTC) and EN 10204 3.1 certification (where applicable)
DB6 Case Study 40% Improvement in Die Life in Forging
Operations Customer Challenge
A drop-forging plant for automotive components experienced premature die cracking of crankshaft forging dies made from standard hot work steels leading to expensive downtime.
Solution
The tooling was upgraded to DB6 (DIN 1.2714) supplied by Virat Special Steels, vacuum heat treated and double tempered to an optimized 46-48 HRC.
Results
40% increased die service life Eliminate catastrophic die cracking in high energy impact Lower maintenance and machine downtime Forged at a lower cost per part
Certifications Available
Reputable suppliers typically provide:
- Mill Test Certificate (MTC)
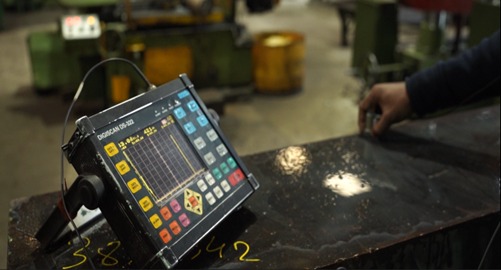
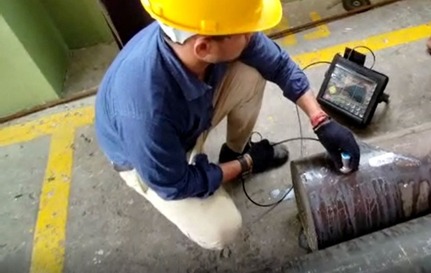
- Ultrasonic Tested Material
- Hardness Test Report
- Chemical Test Report
Buyer’s Guide: Selecting the Appropriate DB6 Tool Steel
Some important points to consider before buying DB6 Tool Steel (DIN 1.2714) to get the best out of your application:
1. Choose the Right Hardness
Pick the hardness for your application:
- 38-42 HRC – Greater toughness and impact resistance
- 50-56 HRC – Increased wear resistance and extended tool life
2. Choose the required form of material
DB6 Tool Steel is supplied in:
- Forged and Rolled blocks
- Round and Flat Bars
- ESR and Non ESR Blocks
3. Material Quality Inspection
Always ask for:
- Mill Test Certificate (MTC) Ultrasonic Tested Material
- Material Traceability Spectro Tested Material
4. Match the App
Select DB6, depending on your tooling needs, such as:
- Forging Dies
- Hammer Dies
- Extrusion
- Holders for
- Casting Dies
5. Select a Trusted Supplier
Join hands with a supplier who can support with ready stock, custom machining, technical support and PAN India delivery for consistent quality and timely supply.
Why purchase DB6 Tool Steel from Virat Steels?
Selecting the right supplier is critical to maximizing tool life, performance and productivity. With over 70 years of experience in the industry, Virat Steels is one of the trusted suppliers of high quality imported and domestic tool steels in India with more than 2000 customers in the automotive, forging, die casting, aerospace, plastic mould, heavy engineering, railways and defence industries.
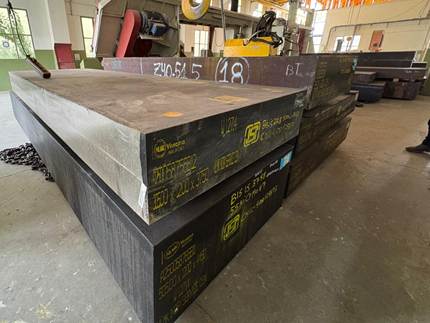
Why do manufacturers trust us?
- 70+ Years Experience supplying quality tool steels.
- 2,000+ Happy Customers in India’s Manufacturing Industry.
- Supplier of Materials from Reputed International Mills for consistent quality and performance.
- Tool Steel Ready Stock: DB6, H13, H11, D2, D3, P20, P20+Ni, M2, M35, EN31, OHNS and other grades.
- Mill Test Certificate (MTC) with full traceability of material.
- UT Tested & Spectro Tested Material for proven quality and internal soundness.
- Custom Cutting & Machining Services to suit your required sizes.
- Material Selection Assistance from experienced technical professionals.
- Fast PAN India Delivery, timely supply & reduced production downtime.
Virat Steels offers authentic quality, certified material and dependable service for all your tool steel needs. Whether DB6 Round Bars, Forged Blocks, ESR Blocks, Flat Blocks or Cut-to-size Material, we have it all.
Our Supply Network Across India
Virat Steels is one of the leading suppliers of DB6 Tool Steel (DIN 1.2714) to the manufacturers in the major industrial hubs of India like Ahmedabad, Rajkot, Pune, Nashik, Aurangabad, Kolhapur, Belgaum, Chennai, Coimbatore, Hosur, Bengaluru, Hyderabad, Faridabad, Manesar, Bhiwadi, Gurugram, Delhi NCR, Ludhiana, Chandigarh, Haryana, Punjab and Jamshedpur.
Our strong logistics network, ready stock and technical knowledge enable us to provide fast PAN India delivery to forging companies, die makers, tool rooms, plastic mould manufacturers, die casting industries and heavy engineering businesses.
Conclusion
DB6 Tool Steel (DIN 1.2714) is a high-performance hot work tool steel, known for its excellent toughness, wear resistance and thermal fatigue resistance. Proper heat treatment gives it hardness in the range of 45–56 HRC and makes it ideal for forging dies, extrusion tooling, die casting dies, and other demanding industrial applications.
Virat Steels is your trusted partner for premium quality DB6 Tool Steel with 70+ years of experience, 2000+ customers, ready stock, MTC, UT & Spectro Tested materials and PAN India delivery.
Call us or send your drawing to receive a customised material recommendation.
Request a Quote
Looking for premium-quality DB6 Tool Steel (DIN 1.2714)?
Virat Steels supplies DB6 Round and Flat Bars & Forged and Rolled Blocks, ESR /non ESR Blocks, Cut-to-Size Material with:
- ✔ 70+ Years of Industry Experience
- ✔ 2,000+ Satisfied Customers
- ✔ Ready Stock
- ✔ MTC Available
- ✔ UT Tested Material
- ✔ Spectro Tested Material
- ✔ Custom Machining
- ✔ PAN India Delivery
Contact Virat Steels today for technical guidance and a customized quotation for your DB6 Tool Steel requirements.
Download PDF:
https://www.viratsteels.com/downloads/DB6_vs_H13_H11_D2_Comparison.pdf
https://www.youtube.com/shorts/qf8SFJDCtlE
https://www.youtube.com/shorts/5hnQ_qp3WsA
Call us: +91-98140 21775 Email: info@viratsteels.com Visit us: Gurgaon (Haryana) | Ludhiana (Punjab)
Frequently Asked Questions
1. What is the working hardness of DB6 steel?
DB6 steel is typically tempered to a working hardness of 44–50 HRC depending on the forging application.
2. Is DB6 a hot work or cold work tool steel?
DB6 (DIN 1.2714) is a premium hot work alloy tool steel containing Nickel, Chromium, Molybdenum, and Vanadium.
3. What is the annealed hardness of DB6?
In annealed condition, DB6 has a hardness of 220–250 HB (Brinell Hardness) for easy machining.
4. What is the hardening temperature for DB6?
The recommended hardening (austenitizing) temperature is 840–870°C followed by oil, polymer, or air quenching.
5. How many tempering cycles are required for DB6?
At least two tempering cycles (double tempering) are required to relieve stress and stabilize the micro-structure.
6. Is DB6 equivalent to D2 or SKD11?
No. DB6 is a hot work steel (1.2714). D2 / SKD11 (1.2379) is a cold work steel used for cold punching and blanking.
7. What is the DIN equivalent of DB6?
The exact DIN equivalent is DIN 1.2714 (55NiCrMoV7) (L6).
8. What makes DB6 tough?
The presence of 1.50–1.80% Nickel (Ni) gives DB6 exceptional core toughness and resistance to impact cracking.
9. Can DB6 be used for blanking dies?
No, cold blanking requires cold work steels like D2 or DC53. DB6 is engineered for hot forging and high-impact dies.
10. What industries rely on DB6 tool steel?
Drop forging, press forging, automotive component manufacturing, heavy engineering, and defense.
11. Is pre-hardened DB6 available?
Yes, DB6 is often supplied in a pre-hardened condition (~35–40 HRC) for direct die cavity machining.
12. Can DB6 steel be welded?
Welding DB6 is difficult due to its high hardenability. Preheating to 300–400°C and post-weld stress relief are essential if welding is necessary.
13. Why does DB6 outperform H13 in drop forging hammer dies?
DB6 has higher Nickel content, offering superior impact energy absorption compared to H13, preventing die shattering under heavy hammer blows.
14. Why is stress relieving important before hardening DB6?
It removes machining stresses, preventing warping and dimensional movement during quenching.
15. What quality reports come with DB6 from Virat Special Steels?
Material Test Certificate (EN 10204 3.1), Ultrasonic Testing (UT) report, and Hardness/Chemical test reports.
16. Does DB6 resist thermal fatigue?
Yes, its balanced Cr-Ni-Mo composition gives high resistance to heat checking (thermal fatigue).
17. What supply forms are available for DB6?
Round bars, flat blocks, forged blocks, and custom cut plates.
18. What is the primary advantage of DB6?
High impact toughness combined with excellent hardenability across large block sizes.
19. What should buyers check before buying DB6?
Ensure ultrasonic soundness (UT testing) to prevent internal defects in large die blocks.
20. Why choose Virat Special Steels for DB6?
Extensive stock, certified quality, precision cutting facilities, quick delivery, and decades of technical expertise.