

D2 steel HRC
now browsing by category
Cut-to-Size Die Blocks: Machining Allowance Guide for DB6, H13, D2 & P20
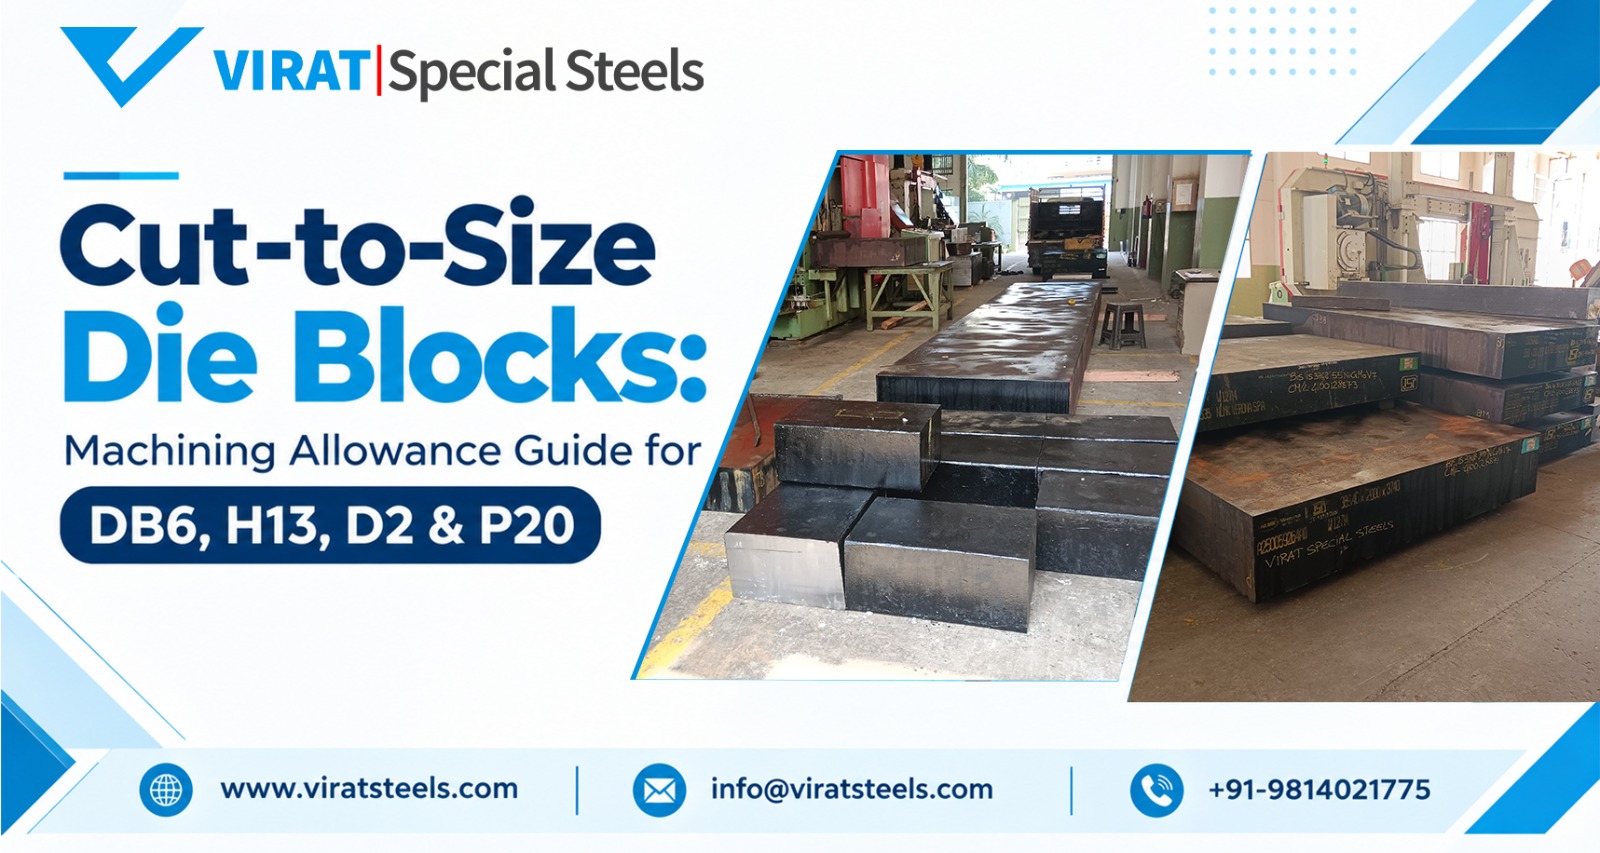
Technical guide by Virat Special Steels · Die and tool steel stockists since 1957
Order a Cut-to-Size Die Blocks with too little allowance and it can’t be cleaned up after heat treatment, so it ends up as scrap. Order too much and you pay for steel, sawing and machine time that turns into chips.
This manual provides us with a summary of the allowance for machining based on the requirements of the various categories from the Indian forging, die-casting, and toolroom industries including DB6 (DIN 1.2714), H13, H11, D2, D3, and P20.
Machining Allowance for Cut-to-Size Die Blocks
Plan these ranges per side (per face), then confirm with your supplier:
| Delivery condition | Allowance per side | What it has to cover |
| Black (hot-rolled or forged) | 3–6 mm for most sizes; more on wide sections | Scale, seams, decarburized skin, bow |
| Saw-cut and rough-milled | 1–2 mm | Remaining geometry error, semi-finishing |
| Six-side milled | 0.2–0.4 mm | Final sizing; standard programmes ship +0.4 to +0.8 mm over nominal overall |
| Precision ground with allowance | 0.15–0.3 mm | Final sizing only |
If hardening is going to be done after machining the piece, allow for at least 0.15% of each dimension on each side for the final finishing of the piece. For instance, a 200 mm face would require about 0.3 mm to be kept.
These figures are based on available data from the mills and actual shop practice; they should not be considered standard values. The actual numbers may depend on the type of alloy, the shape of the section and the method you use. Therefore, make sure to send an engineering drawing before you finish up.
What Is Machining Allowance on a Die Block?
The machining allowance refers to the additional material requested to have the workpiece in its finished form. This is often defined by a number for each side, such as 3 mm per side for a 6 mm allowance in total. With cut-to-size die blocks, you would incorporate this allowance in your order specifications and make sure to mention it on the order.
Breakdown of Machining Allowance Layers
Total allowance is a stack of four layers, and each one exists for a reason.
| Layer | What it covers | Planning figure per side |
| 1. Surface | Scale, seams, laps and the decarburized skin left by hot working | 1.6% of the dimension, usually not under 2 mm |
| 2. Geometry | Bow, camber, out-of-flat and cutting tolerance | 0.3–0.5 mm |
| 3. Heat treatment | Hardening movement, residual scale or decarburization | 0.15% of the dimension, minimum about 0.3 mm |
| 4. Finishing | EDM recast removal, polishing | Small; set by the finishing process |
Layer 1: surface. Hot rolling and forging leave scale, seams and a skin where carbon has burned out. That soft skin won’t harden properly, so it must go. The AISI benchmark for hot-rolled flats and squares is removal of at least 1.6% of the dimension per side (2.4% for resulfurized steel). It was written for carbon and alloy bars, so treat it as a floor for tool steel. Decarburization depth is measured to ASTM E1077 or ISO 3887.
Layer 2: geometry. No bar is perfectly straight or flat, and long pieces bow more. Cutting adds tolerance, and length is the loosest dimension: +3/+8 mm on Uddeholm’s saw-cut stock, up to +35 mm in some precision flat programmes. Never rely on sawn length for a fit.
Layer 3: heat treatment. The sound workflow is rough machine, stress relieve, semi-finish, harden, grind. Uddeholm recommends 650°C for two hours after roughing H13; Virat’s DB6 guidance is 600–650°C. The Böhler-Uddeholm D2 data sheet sets a minimum of 0.15% per side, but only with stress relief, and Uddeholm’s oil-hardening Arne steel lists 0.25%. Movement can be small: on a 100 × 100 × 25 mm H13 sample, thickness changes 0 to +0.05% after air hardening and up to +0.30% after oil hardening. Scale and decarburization from hardening must also be ground off, so the allowance is never just the movement figure.
Layer 4: finishing. Wire EDM leaves a recast layer. Uddeholm advises removing it by grinding or stoning, then re-tempering about 25°C below the previous tempering temperature. Polishing needs little stock.
Formula and Worked Example
Per side: cleanup (the greater of 2 mm or 1.6% of the dimension) + geometry buffer (0.5 mm) + grinding stock (0.15% of the dimension, minimum 0.3 mm). Order size = finished size + 2 × that total.
For instance, a D2 block, which has a final measurement of 250 × 150 × 50 mm owing to the black flat finish, requires a thickness of 4.9, 3.2 and 2.8 mm on each side. This means that one should order something in the order of 260 × 157 × 56 mm with the understanding that this is merely an estimate rather than a guarantee.
Seven mistakes that cost money
- Writing “+5 mm” without saying per side or total.
- Using one allowance for every grade and condition.
- Ignoring bow on long flats.
- Skipping stress relief between roughing and finishing.
- Accepting a gas-cut block to save a few rupees.
- Expecting ESR to shrink the allowance. ESR cleans the inside of the steel. The surface still carries scale and decarb.
- Hoping allowance will fix internal defects. It won’t. For critical blocks, ask for ultrasonic testing.
What to send with your enquiry
- Grade and drawing, with finished size (L × W × T)
- Process route: use as supplied, or harden after machining
- Heat-treatment method: vacuum or atmosphere furnace
- Supply condition wanted: black, milled or ground
- Cutting method and tolerance (saw cut, plus-only or plus-minus)
- Documents needed: MTC, UT, spectro check
- Quantity and delivery location
Specific Scenarios and Add-Ons
Pre-hardened die blocks (DB6, H13, P20). Virat supplies DB6 annealed or hardened and tempered, typically at 38–44 HRC. If you machine the block as supplied, Layer 3 disappears. Keep Layers 1, 2 and 4, and confirm the condition at order stage.
Hardening after machining (D2, D3, soft H13). Use all four layers. Machine soft, stress relieve, harden, then grind.
Wire EDM. Blocks for eroding are often bought hardened and ground, sometimes with start holes. Allow for recast removal and agree finishing stock with your EDM shop.
Flame or plasma-cut blanks. Avoid them for alloy tool steel. Thermal cutting leaves a hardened heat-affected zone and cracking risk, and needs far more stock. Band-sawing is the safer route.
Large forged blocks. Allowance grows with size, so never reuse a 100 mm figure on a 400 mm block. For heavy die blocks, ask for ultrasonic testing. Virat supplies DB6 die blocks with extra forging reduction and double tempering for better UT quality.
Nitriding. Nitrided cases are shallow (about 0.12–0.20 mm in Uddeholm’s H13 examples), so finish the block first and treat nitriding as a surface step, not an allowance layer.
Add-ons to request on your enquiry:
- Bandsaw cut-to-size and surface machining
- Annealed or hardened-and-tempered supply; ESR or non-ESR
- Ultrasonic testing
- Mill Test Certificate (EN 10204 3.1 where applicable), spectro and hardness reports
- Ground reference faces with squareness and parallelism limits
- Batch-wise traceability
Common Material Grades for Cut-to-Size Die Blocks
Allowance logic changes with the grade and its supply condition:
| Grade (AISI / DIN) | Typical use | Allowance note |
| DB6 / 1.2714 (L6) | Hammer and press forging dies | Often supplied hardened and tempered, so no heat-treatment layer |
| H13 / 1.2344 | Die casting, extrusion, hot forging | Air or vacuum hardening keeps movement small; stress relief still applies |
| H11 / 1.2343 | Forging and aluminium extrusion dies | Plan like H13 |
| D2 (HCHCr) / 1.2379 | Blanking and forming dies, punches | Air hardening; keep at least 0.15% per side with stress relief |
| D3 (HCHCr) / 1.2080 | High-abrasion, long-run tooling | Oil hardening; leave more grinding stock than D2 |
| P20 / 1.2311 | Plastic mould blocks | Usually pre-hardened; no heat-treatment layer |
| P20+Ni / 1.2738 | Large mould blocks | Better through-hardening in thick sections |
Sourcing and Customization Options
Virat Special Steels has nearly 3,500 tons in over 35 grades available at its yards in Ludhiana and Gurugram, resulting in large amounts of cut-to-size die blocks shipped out from stock. The billets originate from mills such as Swiss Steel, NLMK Verona, Lucchini and ThyssenKrupp. Blocks reach you in four conditions, each trading price for convenience:
- Saw-cut black block: lowest cost per kg, most allowance to remove.
- Rough-milled: surface layer gone, flatter.
- Six-side milled: close to size, less machining time. Check the stock left if you will harden.
- Hardened and ground: ready for EDM or fitting, with no allowance for further heat treatment.
Include these on your enquiry:
- Grade and delivery condition
- Finished size and order size, stating per side or overall
- Faces to be ground, with tolerances
- Hardening plan and target hardness
- Testing and certificates needed
- Quantity and delivery date
Contact VIRAT for Drawing-Based Sizing and a Quotation
Let us know your engineering drawing, steel grade, dimensions after machining (L x W x T), desired supply condition, volume, and destination point for supply by Virat Special Steels. Our experts will assist you in estimating machining allowance and provide appropriate die blocks as per your needs.
You may get in touch with us at +91-98140 21775 or write to us at info@viratsteels.com to request for a quotation. We manufacture DB6, H13, H11, D2, D3, and P20 tool and die steels from our Gurugram and Ludhiana plants, supplied across India as per availability.
Frequently Asked Questions
1. How much machining allowance should I leave on a die block? Plan 3–6 mm per side on black stock, 1–2 mm on rough-milled and 0.2–0.4 mm on six-side milled blocks, plus grinding stock if you will harden afterwards.
2. Is machining allowance per side or total? Normally per side. A 3 mm allowance adds 6 mm to each dimension, so always state “per side” or “overall” on your enquiry.
3. How much allowance should I keep for grinding after heat treatment? At least 0.15% of the dimension per side for D2 after stress relief. Oil-hardening grades need more; Uddeholm lists 0.25% for its O1-type Arne steel.
4. Do pre-hardened DB6 (DIN 1.2714) die blocks need heat-treatment allowance? Not if you machine them as supplied, typically 38–44 HRC. Keep the surface, geometry and finishing allowances only.
5. What do black, rough-milled and six-side milled mean? Black keeps the as-forged or as-rolled skin. Rough-milled has the skin removed with stock left. Six-side milled is square and parallel, close to final size, so you can start machining straight away.
6. What do “hot die steel”, “HCHCr”, “OHNS” and “die block” mean? Hot die steel is hot-work steel such as H13, H11 and DB6. HCHCr is high-carbon, high-chromium cold-work steel (D2 and D3). OHNS is oil-hardening non-shrinking steel, usually O1. A die block is a large forged or rolled block used for forging and casting dies.
7. Can I flame-cut or plasma-cut a die block? Avoid it for alloy tool steel. These processes will create a hardened heat-affected area, with the possibility of fracture and wasted material. Instead, consider using a band saw.
8. How much stock should I leave for wire EDM? Enough to remove the recast layer by grinding or stoning, followed by re-tempering about 25°C below the last tempering temperature. Agree exact stock with your EDM shop.
9. What tolerance can I expect on cut length? Length is the loosest dimension. Published saw-cut tolerances run from +3/+8 mm to +35 mm, so ask your supplier for its tolerance and never rely on sawn length for a fit.
10. Db6 or H13 for forging die blocks? The typical material for hammering and press dies is DB6 (DIN 1.2714), while H13 (DIN 1.2344) is the preferred alloy for hot-working conditions like die casting, extrusion, and hot forging. This depends on temperature, impact loads, die configuration, and service life.
11. Does D2 or O1 (OHNS) need more allowance? O1, an oil-hardening grade, needs more grinding stock than air-hardening D2. “Non-shrinking” does not mean no movement.
12. Can I buy a small cut piece instead of a full bar? Yes. Virat Special Steels can provide steel that is cut to size depending on the grade, dimensions and availability of stock. Please inform us of your desired dimensions and quantities.
13. Is cut-to-size priced per kg or per piece? Most manufacturers charge according to the overall weight including the costs of cutting and machining. The extra allowance will be reflected in the weight, too, so you should size it accurately and ask them for your cutting estimate.
14. How can I check I received the grade I ordered? Ensure that the heat number on the material marking is the same as stated in the Mill Test Certificate (MTC). Another way would be to ask for an OES analysis to prove the steel grade. Spark testing cannot be considered a reliable way of verifying the alloy tool steel grade.
15. Can I get MTC and ultrasonic testing on cut-to-size blocks? Yes, request them at order stage. Virat supplies MTC (EN 10204 3.1 where applicable), UT-tested material and spectro verification, subject to grade and product.
16. How fast can I get a quotation and delivery? To receive a quotation from Virat Special Steels, share your steel grade, drawing or size, quantity, and the place where the delivery will take place. The lead time varies from time to time, based on availability of material, any cutting/machining work, testing, and transport.
17. How do I calculate die block weight? Length × width × thickness in mm ÷ 1,000,000 × 7.85 gives kg, using a typical tool steel density of 7.85 g/cm³. A 250 × 150 × 50 mm block weighs about 14.7 kg.
18. Where can I buy cut-to-size die blocks in India? Virat Special Steels supplies DB6, H13, H11, D2, D3 and P20 die blocks from ready stock at Ludhiana and Gurugram, with PAN India delivery, subject to grade and size.
D2 vs D3 Material: Composition, Hardness, Properties & Selection Guide
If you manufacture dies, punches, molds or precision tooling, you may need to choose between D2 vs D3 material. Both are high-carbon, high-chromium cold-work tool steels, but their chemical composition, carbide structure, heat-treatment response, toughness, machinability and wear resistance differ.
D2 material contains molybdenum and vanadium and provides a good balance of wear resistance, toughness and dimensional stability. D3 material has higher carbon and carbide content and is generally considered for applications where high abrasion resistance is required and impact loading is relatively low.
In this guide, we compare D2 vs D3 material in terms of chemical composition, hardness, properties, machinability, applications, cost considerations and grade equivalents to help you understand the factors involved in selecting between the two grades.
What Is D2 Material?
D2 material is a type of air-hardening cold work tool steel that has a high carbon content and high chromium content. It is used in making die and punch tools. It has good dimensional stability in heat treatment and excellent wear resistance. It is sometimes called a “semi-stainless” steel because of its relatively high chromium content.
D2 Steel is popular in many industries, from metal stamping and forming to knife making. It offers a good balance of hardness, edge retention and reasonable toughness.
D2 Chemical Composition
Based on Virat Steels’ own AISI D2 technical data, the typical D2 steel chemical composition is:
| Element | Typical % (D2 material composition) |
| Carbon (C) | 1.40 – 1.60% |
| Chromium (Cr) | 11.00 – 13.00% |
| Molybdenum (Mo) | 0.70 – 1.20% |
| Vanadium (V) | 0.50 – 1.10% |
| Manganese (Mn) | 0.10 – 0.60% |
| Silicon (Si) | 0.10 – 0.60% |
| Iron (Fe) | Balance |
D2 has high carbon and chromium content, which results in large volumes of hard carbides being formed, contributing to its excellent abrasion resistance. Vanadium refines the primary grain structure and forms strong carbides which increase wear resistance, edge holding and high temperature strength. Molybdenum increases the hardenability in conjunction with other alloying elements. This Mo + V combo is the big metallurgy difference from D3, and why D2 generally holds a sharper edge longer.
D2 Material Hardness in HRC
This is one of the most searched questions about the grade, so let’s separate the two conditions clearly:
- D2 material hardness in HRC before heat treatment (annealed/as-supplied condition): D2 comes in a soft condition for ease of machining. D2 in the annealed condition is normally 217-255 HB (Brinell) – which is approximately equivalent to low to mid 20’s on the HRC scale, but Brinell is the standard way this soft condition is actually measured and reported.
- D2 hardness after heat treatment (hardened & tempered): D2 hardness after hardening is 58-62 HRC with a tensile strength of approximately 1,900 MPa and a compressive strength of more than 2,700 MPa. Some suppliers quote a maximum hardness closer to 62 HRC.
Thus, if one asks for “d2 hrc” or “d2 hardness in hrc” without mentioning the state of the material, then the correct response would be that “it depends on whether you are referring to the ‘as supplied’ state (which is soft and machinable) or ‘post heat treatment’ state (which is hard).”
D2 Properties & Applications
D2 grade steel is known for:
- High abrasion and wear resistance
- Good dimensional stability during hardening (it’s air-hardening, so distortion is minimal).
- Mo/V carbides offer good edge retention
- Semi-stainless behavior in dry environment (mild corrosion resistance)
- Toughness is relatively lower than shock-resisting grades such as S7
Typical applications:blanking and piercing dies, forming dies, thread rolling dies, punches, shear blades, slitter knives, cold extrusion tooling and wear-critical mold components such as guide pins, wear plates and cavity inserts where abrasion – not impact – is the dominant failure mode.
What Is D3 Material?
D3 grade material (AISI/ASTM D3) is another form of high-carbon and high-chromium cold-work tool steel, but it has completely distinct characteristics when it comes to its quenching process. One of the differences of D3 material from other D-series steels lies in the fact that it does not contain 1% of molybdenum. D3 is oil-quenched instead of air-hardened, but small sections can be vacuum/gas-quenched. This oil-hardening route makes tools made from D3 more susceptible to brittleness during the hardening. Internationally, D3 is equivalent to DIN/Werkstoff 1.2080 (X210Cr12) – also known as SKD1 in Japan and Cr12 in China.
D3 Chemical Composition
| Element | Typical % (D3 material composition) |
| Carbon (C) | ~1.90 – 2.20%* |
| Chromium (Cr) | ~11.00 – 13.50%* |
| Manganese (Mn) | ≤ 0.60% |
| Silicon (Si) | ≤ 0.60% |
| Molybdenum / Vanadium | Not a defining addition (unlike D2) |
| Iron (Fe) | Balance |
D3 has a higher carbon content and about the same chromium content as D2, but without the Mo/V additions . This results in a larger volume of primary chromium carbides . That’s the main reason, D3 usually beats D2 on raw abrasion resistance at the expense of toughness.
D3 Material Hardness in HRC
D3 can be heat treated to 58-64 HRC hardness. This is supported by many independent technical data sources for the grade. Like D2, the material hardness of D3 in HRC is highly dependent on the tempering temperature chosen and the section thickness being hardened — for a given tool, verify the target hardness with your heat treatment partner before nailing down the process route.
In the annealed/as supplied condition D3 is also kept soft for machining, generally in line with the rest of the D-series family, but exact annealed hardness should be verified on the supplier’s certificate rather than assumed.
D3 Properties & Applications
- Superior wear and abrasion resistance – Usually rated better than D2 because of increased carbide volume
- Excellent dimensional stability in heat treatment, size retention almost as good as air hardening types such as D2
- High compression strength
- It is less tough than D2 and more prone to chip when subjected to shock or impact loading
- Due to its abrasion resistance, machining should generally be restricted to finish grinding after hardening
Typical applications: forming rolls, drawing dies, powder compaction tooling and lamination dies as well as blanking dies, punches, shear blades, gages and thread rolling dies. Basically high volume, low shock, high abrasion tooling.
D2 vs D3 Material: Key Differences
| Parameter | D2 Material | D3 Material |
| Standard / Equivalent | AISI D2, DIN 1.2379 | AISI D3, DIN 1.2080 |
| Hardening method | Air-hardening | Oil-hardening (air/vacuum for small sections) |
| Carbon content | 1.40–1.60% | ~1.90–2.20%* |
| Chromium content | 11.00–13.00% | ~11.00–13.50%* |
| Mo / V alloying | Present (0.7–1.2% Mo, 0.5–1.1% V) | Not a defining addition |
| Annealed hardness | ~217–255 HB | Similar soft range (verify per MTC) |
| Hardened hardness | 58–62 HRC | 58–64 HRC |
| Wear resistance | Very good | Excellent (typically higher than D2) |
| Toughness | Better of the two | Lower — more brittle |
| Dimensional stability | Excellent | Good, slightly more distortion risk |
| Machinability | Low | Lower than D2 |
| Corrosion resistance | Mild (semi-stainless behaviour) | Similar chromium level, comparable behaviour |
| Best suited for | Long-run dies, punches, wear parts needing edge retention | High-abrasion, low-impact forming/drawing tooling |
| Relative cost | Generally carries an alloy premium (Mo + V) | Often positioned as the more economical D-series option |
*See composition notes above — verify exact figures with your supplier’s mill certificate.
Machinability: D2 vs D3
Both grades have their reputation as “difficult but worth it” in machinability. D2 has a machinability of about 27% of AISI 1112 steel. This is poor compared to general engineering steels, but typical for high performance tool steels of this class.
D3 is generally considered more difficult to machine than D2, because of its higher carbon content and greater volume of carbides. In practice many fabricators machine D3 in the annealed condition and then rely mainly on grinding to bring it to the hardened state, rather than attempting conventional cutting once the hardness is achieved.
Practical takeaway: D2 is the more forgiving option if you have a lot of machining to do after heat treat. If the bulk of the shaping is done before hardening (with finish grinding done after), the lower machinability of D3 is less of a concern.
Which Industries Use D2 and D3?
The two grades cater to different, though similar, parts of the tool and die market segment:
- Tool & die manufacturing: Blanker, piercer and former dies ( grades D2 and D3)
- Mould manufacturing / injection moulding: Wear plates, guide pins, ejector parts and mold cavities exposed to abrasive plastic or filler material (grade D2 where toughness and machinability are important in addition to wear resistance)
- Metal stamping & press tooling: Long run punches and dies (grade D2 for edge wear; grade D3 for abrasion resistance only)
- Wire and thread rolling: thread rolling dies (both grades)
- Sheet metal forming: forming rolls and drawing dies (D3’s strength)
- Powder metallurgy & compaction tooling: compaction dies (D3)
D2 vs D3: Price Considerations
Pricing is specific to section size, quantity, prevailing raw material and alloy surcharge rates, and finishing requirements (rolled, forged, ground, ESR, etc.). We will not give a fixed figure here as this would quickly become outdated and is order dependent.
For example, in general terms: The inclusion of molybdenum and vanadium in D2 usually makes it a slightly more expensive alloy choice than the D3 alloy, which mostly uses carbon and chromium for its composition. For that reason, the D3 alloy can be marketed as the relatively cheaper high-chromium cold work alloy, while D2 comes at a higher cost due to its superior toughness and machinability properties. A quotation request can be made from the manufacturer regarding your required quantity.
How to Choose Between D2 vs D3 Material?
Use these questions to guide the decision:
- Is toughness or pure wear resistance more critical? If your tool sees any shock loading, impact, or lateral force, lean toward D2 (or reconsider A2/S7 for high-shock jobs). If it’s a steady, high-volume abrasive wear situation with minimal impact, D3’s extra hardness pays off.
- How much post-hardening machining is required? If your design needs precision machining after heat treatment, D2’s better machinability makes it the safer choice.
- What’s your quenching setup? D2’s air-hardening gives more forgiving dimensional control for complex geometries; D3’s oil-hardening needs more careful process control, especially on larger sections.
- What’s the production volume and expected tool life target? For very long die life with less concern about impact, D3’s superior abrasion resistance can extend service intervals.
- What’s the budget? If cost-per-kg is a tight constraint and the application doesn’t demand D2’s toughness, D3 is usually the more economical route.
- Does the component need any corrosion resistance in service? Both offer mild, comparable resistance — neither is a substitute for stainless grades in wet/corrosive environments.
If you’re unsure after weighing these factors, share your drawing and application details with Virat Steels’ technical team — grade selection is easier with a specific load case in front of you rather than generic comparisons.
FAQs: D2 vs D3 Material
- What is the difference between D2 and D3 material? D2 and D3 differ in composition and hardening method: D2 contains added molybdenum and vanadium and is air-hardened, while D3 has higher carbon content, no defining Mo/V addition, and is oil-hardened.
- What is D2 material? D2 Steel is an air hardening tool steel that consists of high carbon and chromium content (AISI D2 / DIN 1.2379).
- What is D2 material’s chemical composition? composition is 1.40–1.60% carbon, 11.00–13.00% chromium, 0.70–1.20% molybdenum, 0.50–1.10% vanadium, plus manganese and silicon in the 0.10–0.60% range.
- What is D2 material hardness in HRC? The D2 material usually attains 58-62 HRC after heat treatment. When it is annealed (or before heat treatment), it is provided in the softer form, which is around 217-255 HB.
- What is D2 material hardness in HRC before heat treatment? D2 material is provided in the soft or annealed state before heat treatment, and hence it is not provided in HRC but is provided in Brinell hardness scale (i.e., roughly 217-255 HB).
- What is D3 material’s hardness in HRC? The hardness of the D3 material in HRC ranges from 58-64 HRC after heat treatment.
- Is D2 or D3 harder? D3 has a slightly higher maximum hardness, up to about 64 HRC, compared to D2’s maximum of around 62 HRC, due to its higher carbon content and carbide volume.
- Which is tougher, D2 or D3? D2 is tougher due to fine, balanced carbide formation, while D3’s higher carbon content makes it less tough.
- Can D2 and D3 be used interchangeably? No. Although D2 and D3 have similar properties, there are differences that make D3 inadequate in certain applications where D2 works fine and vice versa.
- Which is better for injection moulds — D2 or D3? D2 can be used for wear-resistant mould components such as guide parts, wear plates and selected inserts, where good wear resistance, dimensional stability and machinability are required. D3 is generally more suitable for applications where very high abrasion resistance is the primary requirement and impact loading is low. The appropriate grade depends on the mould material, filler content, loading conditions, required hardness and manufacturing process. .
- What is D2 material grade used for? D2 grade is suitable for blanking and piercing dies, forming dies, thread rolling dies, punches, shear blades, and wear-related mold inserts..
- Is D2 a stainless steel? No, it is not stainless steel as it contains sufficient chromium content to resist corrosion in dry environments (also known as “semi-stainless”).
- Why is D3 harder to machine than D2? The carbon content in D3 is higher, and the volume of primary chromium carbides in D3 is higher than that of D2, making it more abrasive but at the same time leading to faster wear of the cutting tools during machining.
- What is the price difference between D2 and D3? The price of D2 is slightly higher than that of D3 since D2 contains molybdenum and vanadium. However, the actual price is dependent on the section size, volume and market prices.
- What are the DIN/international equivalents of D2 and D3? D2 is equivalent to DIN/Werkstoff 1.2379 (X153CrMoV12). D3 is equivalent to DIN/Werkstoff 1.2080 (X210Cr12), known as SKD1 (Japan) and Cr12 (China).
Conclusion
While both D2 and D3 have been confirmed as having high carbon and high chromium content cold work tool steel, it does not mean that they are one and the same only branded differently. The addition of molybdenum and vanadium in D2 makes it tougher and easier to machine, hence it is better used in dies, punches, and die elements. The increased carbon in D3 increases its wear resistance and hardness; however, it reduces toughness.
The right grade depends on your specific load conditions, production volume, and machining process — not a generic “which is better” answer.
Need help selecting between D2 and D3 for your next tooling project? Virat Steels supplies both grades with full mill test certification and technical support to match the right steel to your application. Get in touch with our team for a quote or a grade recommendation based on your drawing.
Our technical team will confirm grade equivalence, available sizes and delivery timeline within 24 hours.
Prefer to talk directly?
Gurugram, Haryana | Ludhiana, PunjabPhone: +91-98140-21775
Email: info@viratsteels.com
Best Cold Work Tool Steel Supplier in India- D2, D3, DIN 1.2379, DIN 2080 Steel | Virat Steels
Premium Cold Work Tool Steel Supplier in India
India’s manufacturing sector is on the rise and the quality of tool steel has a direct impact on productivity, precision and tool life. Premium cold work tool steels are used extensively in automotive, forging, sheet metal and heavy engineering industries, and offer consistent performance and reduced downtime.
With increasing demand for premium grade tool steels across India, Virat Special Steels continues to be a preferred choice for industries looking for reliable quality, imported steel grades, extensive inventory and fast nationwide delivery support.
What is Cold Work Tool Steel?
Cold work tool steel is a group of tool steel that is designed specifically for uses carried out at room temperature. These steels provide a great combination of hardness, wear resistance, toughness and dimensional stability, which makes them suitable for high precision tooling applications.
Key Properties of Cold Work Tool Steel
- High hardness
- Excellent wear resistance
- Superior edge retention
- High compressive strength
- Good dimensional stability
- Enhanced toughness
Applications of Cold Work Tool Steel
Cold work tool steels are extensively used in:
- Punches and dies
- Blanking dies
- Forming tools
- Shearing blades
- Precision cutting tools
- Industrial knives
- Stamping tools
- Thread rolling dies
- Extrusion Dies
- Burnishing Tools
- Heading Tools
- Coining Dies
Why Cold Work Tool Steel is Important in Manufacturing
Modern manufacturing industries require tooling materials that provide precision, durability and reliable performance. These are the benefits of cold work tool steels, which also bring lower maintenance costs and less production downtime.
| Benefit | Industrial Advantage |
| High Wear Resistance | Longer tool life |
| High Hardness | Better cutting and forming performance |
| Dimensional Stability | Improved manufacturing accuracy |
| Superior Toughness | Reduced cracking and chipping |
| Good Machinability | Easier processing and fabrication |
| Cost Efficiency | Lower maintenance and replacement costs |
Why Choosing the Right Tool Steel Supplier Matters
Choosing the right tool steel supplier is as important as choosing the right steel grades. A dependable supplier provides material consistency, quality assurance and technical support that directly impact tooling performance.
Key Factors to Consider
| Factor | Importance |
| Genuine Steel Grades | Prevents premature tool failure |
| Ready Stock Availability | Ensures uninterrupted production |
| Technical Expertise | Helps select the correct steel grade |
| Fast Delivery Support | Minimizes downtime |
| Quality Assurance | Guarantees certified material quality |
| Competitive Pricing | Improves overall project economics |
Popular Cold Work Tool Steel Grades Available at Virat Special Steels
Virat Special Steels supplies a wide range of imported and premium cold work tool steels, including:
D2 Tool Steel
One of the most widely used cold work tool steels known for excellent wear resistance, hardness, and dimensional stability.
D3 Tool Steel
Suitable for applications requiring maximum wear resistance and excellent edge retention.
DIN 1.2379 Steel
A premium chromium-rich cold work tool steel widely used for precision dies, blanking tools, and cutting applications.
Heat Treatment
The heat treatment process involves carefully controlled parameters such as heating temperature, heating and cooling rates, soaking time, furnace type, quenching medium, and workpiece transfer facilities. These factors are critical for achieving the desired metallurgical properties, including high hardness, excellent wear resistance, and dimensional stability, making the material suitable for demanding tooling applications such as dies, punches, shear blades, and molds.
- Preheating – Heat gradually to about 650–850°C temperature to reduce thermal shock.
- Austenitizing (Hardening) – Heat to the recommended hardening temperature typically 950–1050°C, depending on the grade and hold until the structure becomes austenitic.
- Quenching – Cool rapidly in air, oil, or salt bath (depending on the steel grade) to obtain high hardness.
- Tempering – Reheat to 150–550°C temperature and hold for a specified time, then cool which reduces brittleness and improves toughness while maintaining hardness.
- Stress Relieving – For machined parts, stress relief may be performed before hardening to minimize distortion.
How to Select the Right Cold Work Tool Steel
Choosing the correct cold work tool steel depends on multiple factors:
Consider the Application
Different applications require different combinations of hardness, toughness, and wear resistance.
Evaluate Wear Resistance Requirements
High-production environments often require steel such as D2 or DIN 1.2379 for longer tool life.
Assess Toughness Requirements
Applications prone to impact loading may require tougher grades such as DC53.
Review Machinability
The selected steel should support efficient machining and heat treatment processes.
Seek Expert Technical Guidance
Working with experienced suppliers such as Virat Special Steels ensures optimal material selection based on specific manufacturing requirements.
Conclusion
Cold work tool steels are the backbone of precision, durability and efficiency in modern manufacturing operations. The selection of steel grade and supplier directly impacts tool life, productivity and operational cost savings.
Virat Special Steels is one of the trusted suppliers of tool steels in India offering premium quality high-performance cold work tool steels like D2, D3, DIN 1.2379, DIN 2080, DC53 and other grades. With wide range of inventory, technical expertise, quality assurance and Pan India delivery support, Virat Special Steels continues to be the choice of manufacturers across different industries.
Looking for reliable cold work steel solutions?
Contact Virat Special Steels today for expert guidance and premium tool steel supply.
+91 98140-21775 info@viratsteels.com
For more details about our cold work tool steel grades and applications, please click on the link below to explore our product range and technical specifications.
https://www.viratsteels.com/cold-work-steel.html
https://www.viratsteels.com/hchcr-d2.html
https://www.viratsteels.com/hchcr-d3.html
Frequently Asked Questions (FAQs)
1-What is cold work tool steel?
Cold work tool steel is a type of tool steel used for applications performed at room temperature. It offers excellent hardness, wear resistance, and durability.
2-Which industries use cold work tool steel?
Automotive, forging, sheet metal, aerospace, railway, defence, hand tools, and precision engineering industries commonly use cold work tool steels.
3-Which is the most popular cold work tool steel grade?
D2 tool steel is one of the most widely used grades because of its excellent wear resistance and long service life.
4-What is DIN 1.2379 steel used for?
DIN 1.2379 steel is commonly used for blanking dies, punches, industrial knives, cutting tools, and precision tooling applications.
5-Why are imported tool steels preferred?
Imported tool steels often provide superior quality consistency, improved toughness, better wear resistance, and extended tool life.
6-Which supplier in India is best for cold work steels?
Virat Special Steels offers genuine imported steel grades, ready stock availability, technical support, quality assurance, and fast delivery across India.
7-Why choose Virat Special Steels for cold work tool steel?
Virat Special Steels offers genuine imported steel grades, ready stock availability, technical support, quality assurance, and fast delivery across India.
8-How do I select the right cold work tool steel grade?
Selection depends on application requirements, hardness, toughness, wear resistance, production volume, and expected tool life.
Hardness Ratings (HRC) in Tool and Die Steel
Virat Steels | India’s Leading Tool and Die Steel Supplier
Virat Steels | India’s Leading Tool and Die Steel Supplier
If you’ve ever looked at a tool steel datasheet and wondered what “58 HRC” means and why it matters for your die or mould. Hardness is one of the most critical properties in tool and die steel selection. Get it right, and your tooling performs reliably for thousands of production cycles. Get it wrong, and you’re facing premature wear, unexpected cracking, or both. This complete blog explains what is the Rockwell C scale means, maps HRC ranges to every major tool steel grade, and shows you exactly how to choose the right hardness for your application.
What is Hardness in Steel and Why Does It Matter?
In simple terms, hardness is a material’s ability to resist dents, scratches, or permanent deformation under pressure.
For tool and die steel, hardness is one of the most important properties because it affects:
- Wear resistance – resists abrasion and surface wear
- Edge retention – keeps cutting tools sharper for longer
- Compressive strength – withstands heavy forming pressure
- Dimensional stability – maintains shape and accuracy during production
However, hardness always comes with a trade-off: toughness.
As hardness increases, the steel can become more brittle and prone to cracking under impact.
So, the right steel grade and hardness level should provide the best balance of wear resistance and toughness for the application.
What is the Rockwell Hardness Test?
The Rockwell hardness test is the most widely used hardness measurement method in the tool steel industry.
The Rockwell hardness test checks how hard a material is by measuring how deep a diamond cone goes into its surface.
It works in 3 simple steps:
- Minor load applied – A small force (10 kgf) is applied first to set the starting point and remove surface unevenness.
- Major load applied – A bigger force (150 kgf for HRC) pushes the diamond into the material.
- Load removed – The big force is removed, and the machine measures how deep the mark remains.
Result:
- Less depth = harder material = higher HRC
- More depth = softer material = lower HRC
Understanding HRC -The Rockwell C Scale
HRC stands for Hardness Rockwell C -meaning the result was obtained using the Rockwell C scale. It is the standard unit used to express the hardness of virtually all tool and die steels.
The HRC scale for tool steels runs approximately from 20 HRC(soft, annealed or pre-hardened low-alloy steel) to 68 HRC (the upper limit of conventional hardened tool steel). Here is how the HRC range maps to practical tool steel conditions:
| HRC Range | Condition / Category | In Practice |
| 20-35HRC | Soft / pre-hardened | Easily machined; P20 mould steel supply condition |
| 36-44 HRC | Medium Hardness | Good toughness; forging dies for heavy impact |
| 45-52 HRC | Hard | Balanced wear resistance and toughness; H13 die casting dies |
| 53-60 HRC | Very Hard | High wear resistance; D2 cold work dies, punches |
| 61-66 HRC | Extremely Hard | Maximum wear resistance; M2, M42 high-speed steel cutting tools |
| Above 66 HRC | Ultra Hard | Extremely brittle; not typical for standard die steels |
HRC vs HRB vs HRA — Which Scale Applies to Tool Steel and Die steels?
| HRC | HRB | HRA |
| Indenter: Diamond cone | Indenter: 1/16″ steel ball | Indenter: Diamond cone |
| Major load: 150 kgf | Major load: 100 kgf | Major load: 60 kgf |
| Range: Approx 20–70 HRC | Range: Approx 0–100 HRB | Range: for very hard materials |
| Used For: All hardened and heat-treated tool steels, die steels, high-speed steels, and hardened alloy steels | Used For: Softer steels (mild steel, annealed low-alloy steel), copper alloys, aluminium alloys | Used For: Cemented carbides, case-hardened surfaces, thin hardened layers |
You cannot directly compare numbers from different Rockwell scales. 60 HRC and 60 HRB are not equivalent, they refer to completely different hardness levels. Always confirm which scale a hardness value is expressed in before comparing materials.
HRC vs Brinell (HB) vs Vickers (HV): Approximate conversion table for tool steel
While HRC is the standard for tool steel, you will also encounter Brinell (HB or HBW) and Vickers (HV) hardness values — particularly on material certificates from European suppliers who use DIN specifications.
| HRC | HB (Brinell) | HV (Vickers) | Approx. Tensile Strength |
| 20 | 226 | 238 | ~780 MPa |
| 25 | 253 | 266 | ~870 MPa |
| 30 | 286 | 302 | ~995 MPa |
| 35 | 327 | 345 | ~1140 MPa |
| 40 | 371 | 392 | ~1310 MPa |
| 45 | 421 | 446 | ~1500 MPa |
| 48 | 455 | 481 | ~1630 MPa |
| 50 | 481 | 509 | ~1720 MPa |
| 52 | 512 | 544 | ~1820 MPa |
| 55 | 560 | 595 | ~1980 MPa |
| 58 | 615 | 655 | ~2160 MPa |
| 60 | 654 | 697 | ~2280 MPa |
| 62 | 746 | 746 | ~2400 MPa |
*Note: These are approximate conversions. For precise engineering calculations, always use the original test method. Conversion between hardness scales involves empirical estimates, not exact equivalences. *
HRC Ranges for Common Applications — Quick Reference
If you are selecting tool steel hardness based on the application & the grade, here is a practical quick-reference guide:
| Application | Recommended HRC | Recommended Grade |
| Aluminium die inserts | 44–48 HRC | H13 tool steel / DIN 1.2344 ESR |
| Aluminium extrusion dies | 48–52 HRC | H13 tool steel / DIN 1.2344 |
| Hot forging dies (heavy hammers) | 40–45 HRC | H13 or H11 |
| Hot forging dies (mechanical press) | 46–50 HRC | H13 |
| Cold stamping and blanking dies | 58–62 HRC | D2 tool steel / DIN 1.2379 |
| Cold forming and bending dies | 56–60 HRC | D2 or A2 |
| Plastic injection mould cavities | 48–54 HRC | H13 or P20+Ni |
| Plastic injection mould bases | 28–32 HRC | P20 / DIN 1.2311 |
| Drill bits and taps | 62–65 HRC | M2 / DIN 3343 |
| Cutting and slitting knives | 58–62 HRC | D2 or M2 |
| Punches (light impact) | 58–62 HRC | D2 |
| Punches (heavy impact) | 52–58 HRC | H13 |
| Gauges and measuring tools | 58–64 HRC | D2 or EN31 |
What Happens if HRC is Too High or Too Low?
1. If HRC is too high
The die becomes too hard and brittle.
- More chances of cracking or breaking under impact or stress
- In hot work, heat checking (small surface cracks) starts earlier
- Sharp corners and weak areas may fracture suddenly
- Failure can happen without warning
2. If HRC is too low
The die becomes too soft.
- Surface wears out quickly
- Shape and size accuracy reduce over time
- Can deform permanently under heavy pressure
- In die casting, molten metal may stick to the die (soldering)
- In cutting/stamping, edges become dull or chip fast
- Failure is gradual, but die life becomes much shorter
So, the correct HRC should balance hardness and toughness for the application.
What to check on the MTC
1. Verify the hardness is within the specification for the supply condition. H13 in annealed supply should not exceed 229 HBW. Higher values may indicate the material was not properly annealed.
2. Check for uniformity. If multiple hardness readings are reported from different locations in the bar, they should be consistent. Large variation in hardness across a section is a warning sign of segregation or poor annealing.
3. Confirm the test method. Brinell (HBW) and Vickers (HV) hardness values on the certificate are not directly comparable to HRC values you may see on a datasheet — use the conversion table above if comparison is needed.
4. For pre-hardened grades (P20): Verify the HRC range corresponds to 28–32 HRC. Values outside this range may indicate the steel will machine differently than expected or may not meet the performance requirements of the mould design.
Frequently Asked Questions
1. What HRC stands for in steel?
HRC stands for Hardness Rockwell C, a standard hardness scale for hardened tool steels. Higher HRC means harder and more wear-resistant steel.
2. What HRC is H13 tool steel?
H13 is typically hardened to 40–52 HRC depending on use:
- Die casting: 44–48 HRC
- Extrusion/plastic moulds: 48–52 HRC
- Forging dies: 40–44 HRC
3. What is the HRC of D2 steel?
D2 is usually hardened to 55–62 HRC for stamping and blanking applications.
4. What is the difference between HRC and HB hardness?
HRC uses a diamond cone and measures depth; HB (Brinell) uses a ball indenter and measures impression size.
5. Is higher HRC always better for dies?
No. Higher HRC improves wear resistance but reduces toughness, increasing crack risk.
6. What HRC should I specify for a plastic injection mould?
- P20: 28–32 HRC
- H13: 48–52 HRC for longer runs or abrasive materials
7. Can I check tool steel hardness without a lab?
Yes. Use portable Rockwell or Leeb hardness testers for quick on-site checking.
8. What hardness should I specify when ordering H13?
H13 is usually supplied soft-annealed (max 229 HBW) for machining or can be supplied pre-hardened (30–36 HRC) / fully hardened as required.
9. Why do two steels with the same HRC perform differently?
HRC alone doesn’t tell the full story & performance also depends on:
- Chemical composition
- Heat treatment quality
- Grain structure
- Alloying elements
10. What is the HRC of DB6 steel for forging dies?
For forging dies, DB6 is commonly used around 38–42 HRC to balance toughness and wear resistance. It is known for better toughness than H13 in heavy-impact applications.
- Pre-hardened condition: 360–430 BHN (approx. 38–45 HRC)
- Fully hardened / heat-treated: up to 50–55 HRC
- Annealed condition: max 240–255 BHN
Conclusion
At Virat Steels, we help customers across India choose the right tool steel grade, correct HRC, and suitable size/form for die casting, forging, extrusion, and plastic moulding applications backed by stock availability, test certificates, and ultrasonic-tested material.
📞+91 98140-21775 | 🌐 www.viratsteels.com | ✉ info@viratsteels.com