

Machining Allowance Guide
now browsing by tag
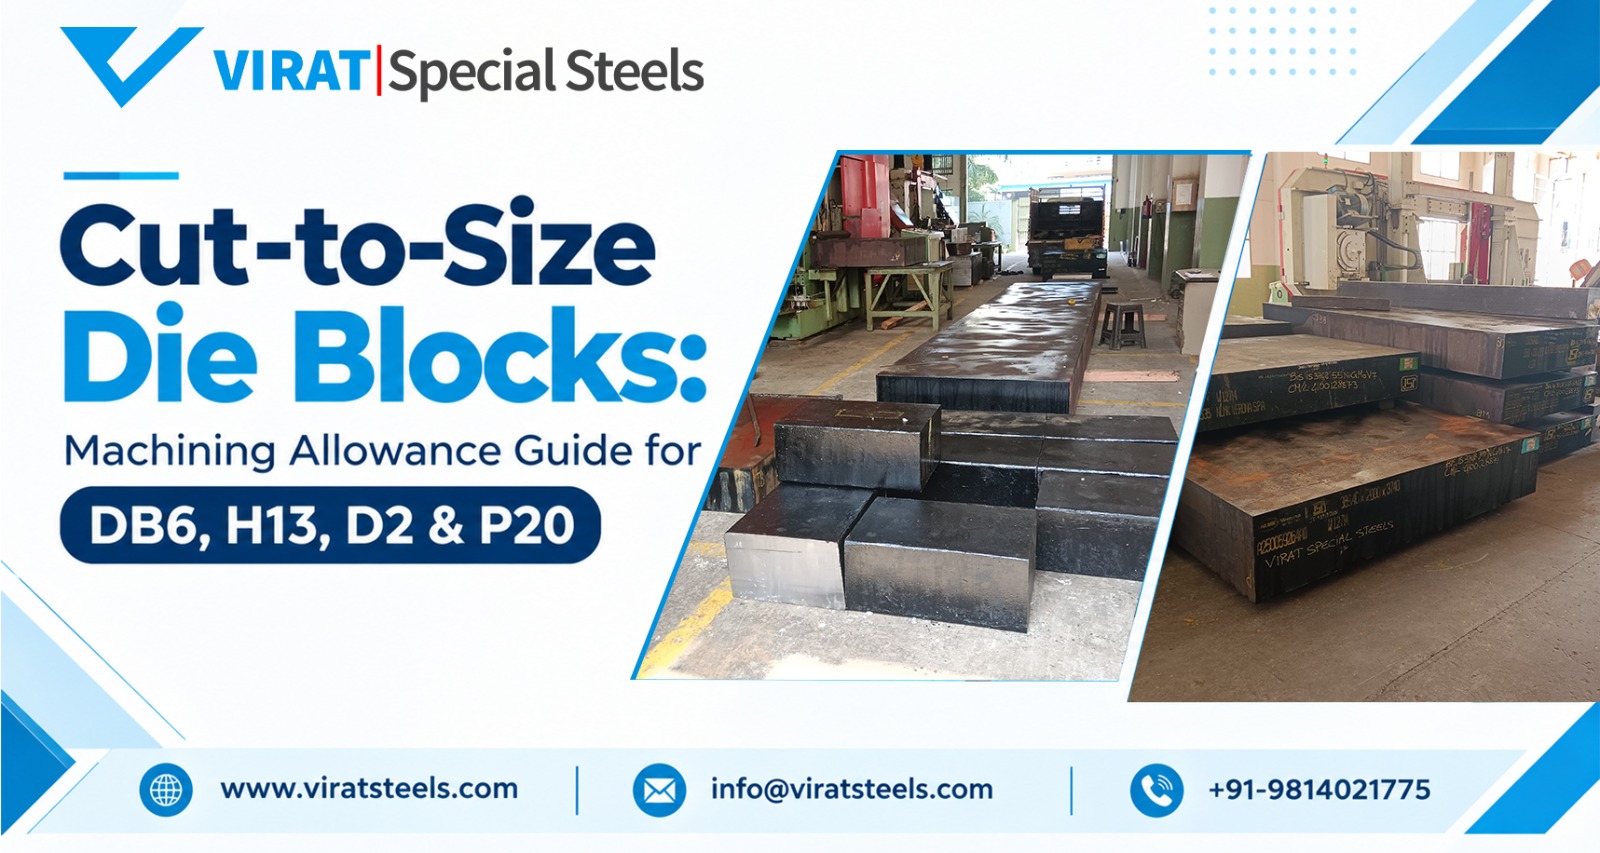
Cut-to-Size Die Blocks: Machining Allowance Guide for DB6, H13, D2 & P20
Technical guide by Virat Special Steels · Die and tool steel stockists since 1957
Order a Cut-to-Size Die Blocks with too little allowance and it can’t be cleaned up after heat treatment, so it ends up as scrap. Order too much and you pay for steel, sawing and machine time that turns into chips.
This manual provides us with a summary of the allowance for machining based on the requirements of the various categories from the Indian forging, die-casting, and toolroom industries including DB6 (DIN 1.2714), H13, H11, D2, D3, and P20.
Machining Allowance for Cut-to-Size Die Blocks
Plan these ranges per side (per face), then confirm with your supplier:
| Delivery condition | Allowance per side | What it has to cover |
| Black (hot-rolled or forged) | 3–6 mm for most sizes; more on wide sections | Scale, seams, decarburized skin, bow |
| Saw-cut and rough-milled | 1–2 mm | Remaining geometry error, semi-finishing |
| Six-side milled | 0.2–0.4 mm | Final sizing; standard programmes ship +0.4 to +0.8 mm over nominal overall |
| Precision ground with allowance | 0.15–0.3 mm | Final sizing only |
If hardening is going to be done after machining the piece, allow for at least 0.15% of each dimension on each side for the final finishing of the piece. For instance, a 200 mm face would require about 0.3 mm to be kept.
These figures are based on available data from the mills and actual shop practice; they should not be considered standard values. The actual numbers may depend on the type of alloy, the shape of the section and the method you use. Therefore, make sure to send an engineering drawing before you finish up.
What Is Machining Allowance on a Die Block?
The machining allowance refers to the additional material requested to have the workpiece in its finished form. This is often defined by a number for each side, such as 3 mm per side for a 6 mm allowance in total. With cut-to-size die blocks, you would incorporate this allowance in your order specifications and make sure to mention it on the order.
Breakdown of Machining Allowance Layers
Total allowance is a stack of four layers, and each one exists for a reason.
| Layer | What it covers | Planning figure per side |
| 1. Surface | Scale, seams, laps and the decarburized skin left by hot working | 1.6% of the dimension, usually not under 2 mm |
| 2. Geometry | Bow, camber, out-of-flat and cutting tolerance | 0.3–0.5 mm |
| 3. Heat treatment | Hardening movement, residual scale or decarburization | 0.15% of the dimension, minimum about 0.3 mm |
| 4. Finishing | EDM recast removal, polishing | Small; set by the finishing process |
Layer 1: surface. Hot rolling and forging leave scale, seams and a skin where carbon has burned out. That soft skin won’t harden properly, so it must go. The AISI benchmark for hot-rolled flats and squares is removal of at least 1.6% of the dimension per side (2.4% for resulfurized steel). It was written for carbon and alloy bars, so treat it as a floor for tool steel. Decarburization depth is measured to ASTM E1077 or ISO 3887.
Layer 2: geometry. No bar is perfectly straight or flat, and long pieces bow more. Cutting adds tolerance, and length is the loosest dimension: +3/+8 mm on Uddeholm’s saw-cut stock, up to +35 mm in some precision flat programmes. Never rely on sawn length for a fit.
Layer 3: heat treatment. The sound workflow is rough machine, stress relieve, semi-finish, harden, grind. Uddeholm recommends 650°C for two hours after roughing H13; Virat’s DB6 guidance is 600–650°C. The Böhler-Uddeholm D2 data sheet sets a minimum of 0.15% per side, but only with stress relief, and Uddeholm’s oil-hardening Arne steel lists 0.25%. Movement can be small: on a 100 × 100 × 25 mm H13 sample, thickness changes 0 to +0.05% after air hardening and up to +0.30% after oil hardening. Scale and decarburization from hardening must also be ground off, so the allowance is never just the movement figure.
Layer 4: finishing. Wire EDM leaves a recast layer. Uddeholm advises removing it by grinding or stoning, then re-tempering about 25°C below the previous tempering temperature. Polishing needs little stock.
Formula and Worked Example
Per side: cleanup (the greater of 2 mm or 1.6% of the dimension) + geometry buffer (0.5 mm) + grinding stock (0.15% of the dimension, minimum 0.3 mm). Order size = finished size + 2 × that total.
For instance, a D2 block, which has a final measurement of 250 × 150 × 50 mm owing to the black flat finish, requires a thickness of 4.9, 3.2 and 2.8 mm on each side. This means that one should order something in the order of 260 × 157 × 56 mm with the understanding that this is merely an estimate rather than a guarantee.
Seven mistakes that cost money
- Writing “+5 mm” without saying per side or total.
- Using one allowance for every grade and condition.
- Ignoring bow on long flats.
- Skipping stress relief between roughing and finishing.
- Accepting a gas-cut block to save a few rupees.
- Expecting ESR to shrink the allowance. ESR cleans the inside of the steel. The surface still carries scale and decarb.
- Hoping allowance will fix internal defects. It won’t. For critical blocks, ask for ultrasonic testing.
What to send with your enquiry
- Grade and drawing, with finished size (L × W × T)
- Process route: use as supplied, or harden after machining
- Heat-treatment method: vacuum or atmosphere furnace
- Supply condition wanted: black, milled or ground
- Cutting method and tolerance (saw cut, plus-only or plus-minus)
- Documents needed: MTC, UT, spectro check
- Quantity and delivery location
Specific Scenarios and Add-Ons
Pre-hardened die blocks (DB6, H13, P20). Virat supplies DB6 annealed or hardened and tempered, typically at 38–44 HRC. If you machine the block as supplied, Layer 3 disappears. Keep Layers 1, 2 and 4, and confirm the condition at order stage.
Hardening after machining (D2, D3, soft H13). Use all four layers. Machine soft, stress relieve, harden, then grind.
Wire EDM. Blocks for eroding are often bought hardened and ground, sometimes with start holes. Allow for recast removal and agree finishing stock with your EDM shop.
Flame or plasma-cut blanks. Avoid them for alloy tool steel. Thermal cutting leaves a hardened heat-affected zone and cracking risk, and needs far more stock. Band-sawing is the safer route.
Large forged blocks. Allowance grows with size, so never reuse a 100 mm figure on a 400 mm block. For heavy die blocks, ask for ultrasonic testing. Virat supplies DB6 die blocks with extra forging reduction and double tempering for better UT quality.
Nitriding. Nitrided cases are shallow (about 0.12–0.20 mm in Uddeholm’s H13 examples), so finish the block first and treat nitriding as a surface step, not an allowance layer.
Add-ons to request on your enquiry:
- Bandsaw cut-to-size and surface machining
- Annealed or hardened-and-tempered supply; ESR or non-ESR
- Ultrasonic testing
- Mill Test Certificate (EN 10204 3.1 where applicable), spectro and hardness reports
- Ground reference faces with squareness and parallelism limits
- Batch-wise traceability
Common Material Grades for Cut-to-Size Die Blocks
Allowance logic changes with the grade and its supply condition:
| Grade (AISI / DIN) | Typical use | Allowance note |
| DB6 / 1.2714 (L6) | Hammer and press forging dies | Often supplied hardened and tempered, so no heat-treatment layer |
| H13 / 1.2344 | Die casting, extrusion, hot forging | Air or vacuum hardening keeps movement small; stress relief still applies |
| H11 / 1.2343 | Forging and aluminium extrusion dies | Plan like H13 |
| D2 (HCHCr) / 1.2379 | Blanking and forming dies, punches | Air hardening; keep at least 0.15% per side with stress relief |
| D3 (HCHCr) / 1.2080 | High-abrasion, long-run tooling | Oil hardening; leave more grinding stock than D2 |
| P20 / 1.2311 | Plastic mould blocks | Usually pre-hardened; no heat-treatment layer |
| P20+Ni / 1.2738 | Large mould blocks | Better through-hardening in thick sections |
Sourcing and Customization Options
Virat Special Steels has nearly 3,500 tons in over 35 grades available at its yards in Ludhiana and Gurugram, resulting in large amounts of cut-to-size die blocks shipped out from stock. The billets originate from mills such as Swiss Steel, NLMK Verona, Lucchini and ThyssenKrupp. Blocks reach you in four conditions, each trading price for convenience:
- Saw-cut black block: lowest cost per kg, most allowance to remove.
- Rough-milled: surface layer gone, flatter.
- Six-side milled: close to size, less machining time. Check the stock left if you will harden.
- Hardened and ground: ready for EDM or fitting, with no allowance for further heat treatment.
Include these on your enquiry:
- Grade and delivery condition
- Finished size and order size, stating per side or overall
- Faces to be ground, with tolerances
- Hardening plan and target hardness
- Testing and certificates needed
- Quantity and delivery date
Contact VIRAT for Drawing-Based Sizing and a Quotation
Let us know your engineering drawing, steel grade, dimensions after machining (L x W x T), desired supply condition, volume, and destination point for supply by Virat Special Steels. Our experts will assist you in estimating machining allowance and provide appropriate die blocks as per your needs.
You may get in touch with us at +91-98140 21775 or write to us at info@viratsteels.com to request for a quotation. We manufacture DB6, H13, H11, D2, D3, and P20 tool and die steels from our Gurugram and Ludhiana plants, supplied across India as per availability.
Frequently Asked Questions
1. How much machining allowance should I leave on a die block? Plan 3–6 mm per side on black stock, 1–2 mm on rough-milled and 0.2–0.4 mm on six-side milled blocks, plus grinding stock if you will harden afterwards.
2. Is machining allowance per side or total? Normally per side. A 3 mm allowance adds 6 mm to each dimension, so always state “per side” or “overall” on your enquiry.
3. How much allowance should I keep for grinding after heat treatment? At least 0.15% of the dimension per side for D2 after stress relief. Oil-hardening grades need more; Uddeholm lists 0.25% for its O1-type Arne steel.
4. Do pre-hardened DB6 (DIN 1.2714) die blocks need heat-treatment allowance? Not if you machine them as supplied, typically 38–44 HRC. Keep the surface, geometry and finishing allowances only.
5. What do black, rough-milled and six-side milled mean? Black keeps the as-forged or as-rolled skin. Rough-milled has the skin removed with stock left. Six-side milled is square and parallel, close to final size, so you can start machining straight away.
6. What do “hot die steel”, “HCHCr”, “OHNS” and “die block” mean? Hot die steel is hot-work steel such as H13, H11 and DB6. HCHCr is high-carbon, high-chromium cold-work steel (D2 and D3). OHNS is oil-hardening non-shrinking steel, usually O1. A die block is a large forged or rolled block used for forging and casting dies.
7. Can I flame-cut or plasma-cut a die block? Avoid it for alloy tool steel. These processes will create a hardened heat-affected area, with the possibility of fracture and wasted material. Instead, consider using a band saw.
8. How much stock should I leave for wire EDM? Enough to remove the recast layer by grinding or stoning, followed by re-tempering about 25°C below the last tempering temperature. Agree exact stock with your EDM shop.
9. What tolerance can I expect on cut length? Length is the loosest dimension. Published saw-cut tolerances run from +3/+8 mm to +35 mm, so ask your supplier for its tolerance and never rely on sawn length for a fit.
10. Db6 or H13 for forging die blocks? The typical material for hammering and press dies is DB6 (DIN 1.2714), while H13 (DIN 1.2344) is the preferred alloy for hot-working conditions like die casting, extrusion, and hot forging. This depends on temperature, impact loads, die configuration, and service life.
11. Does D2 or O1 (OHNS) need more allowance? O1, an oil-hardening grade, needs more grinding stock than air-hardening D2. “Non-shrinking” does not mean no movement.
12. Can I buy a small cut piece instead of a full bar? Yes. Virat Special Steels can provide steel that is cut to size depending on the grade, dimensions and availability of stock. Please inform us of your desired dimensions and quantities.
13. Is cut-to-size priced per kg or per piece? Most manufacturers charge according to the overall weight including the costs of cutting and machining. The extra allowance will be reflected in the weight, too, so you should size it accurately and ask them for your cutting estimate.
14. How can I check I received the grade I ordered? Ensure that the heat number on the material marking is the same as stated in the Mill Test Certificate (MTC). Another way would be to ask for an OES analysis to prove the steel grade. Spark testing cannot be considered a reliable way of verifying the alloy tool steel grade.
15. Can I get MTC and ultrasonic testing on cut-to-size blocks? Yes, request them at order stage. Virat supplies MTC (EN 10204 3.1 where applicable), UT-tested material and spectro verification, subject to grade and product.
16. How fast can I get a quotation and delivery? To receive a quotation from Virat Special Steels, share your steel grade, drawing or size, quantity, and the place where the delivery will take place. The lead time varies from time to time, based on availability of material, any cutting/machining work, testing, and transport.
17. How do I calculate die block weight? Length × width × thickness in mm ÷ 1,000,000 × 7.85 gives kg, using a typical tool steel density of 7.85 g/cm³. A 250 × 150 × 50 mm block weighs about 14.7 kg.
18. Where can I buy cut-to-size die blocks in India? Virat Special Steels supplies DB6, H13, H11, D2, D3 and P20 die blocks from ready stock at Ludhiana and Gurugram, with PAN India delivery, subject to grade and size.