

DB6 Die Block Supplier
now browsing by tag
Cut-to-Size Die Blocks: Machining Allowance Guide for DB6, H13, D2 & P20
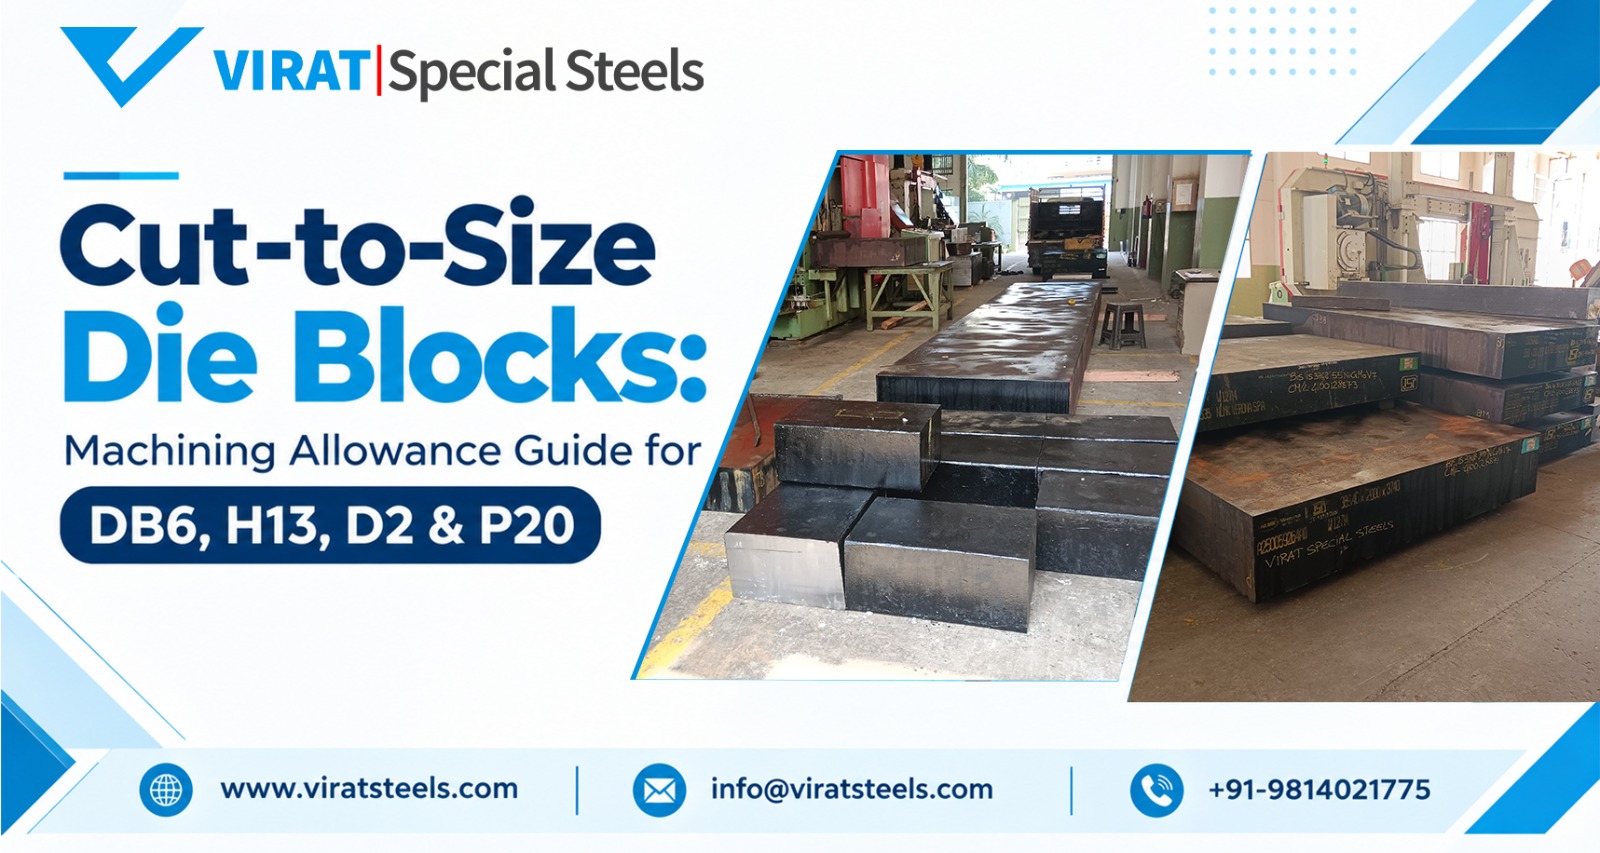
Technical guide by Virat Special Steels · Die and tool steel stockists since 1957
Order a Cut-to-Size Die Blocks with too little allowance and it can’t be cleaned up after heat treatment, so it ends up as scrap. Order too much and you pay for steel, sawing and machine time that turns into chips.
This manual provides us with a summary of the allowance for machining based on the requirements of the various categories from the Indian forging, die-casting, and toolroom industries including DB6 (DIN 1.2714), H13, H11, D2, D3, and P20.
Machining Allowance for Cut-to-Size Die Blocks
Plan these ranges per side (per face), then confirm with your supplier:
| Delivery condition | Allowance per side | What it has to cover |
| Black (hot-rolled or forged) | 3–6 mm for most sizes; more on wide sections | Scale, seams, decarburized skin, bow |
| Saw-cut and rough-milled | 1–2 mm | Remaining geometry error, semi-finishing |
| Six-side milled | 0.2–0.4 mm | Final sizing; standard programmes ship +0.4 to +0.8 mm over nominal overall |
| Precision ground with allowance | 0.15–0.3 mm | Final sizing only |
If hardening is going to be done after machining the piece, allow for at least 0.15% of each dimension on each side for the final finishing of the piece. For instance, a 200 mm face would require about 0.3 mm to be kept.
These figures are based on available data from the mills and actual shop practice; they should not be considered standard values. The actual numbers may depend on the type of alloy, the shape of the section and the method you use. Therefore, make sure to send an engineering drawing before you finish up.
What Is Machining Allowance on a Die Block?
The machining allowance refers to the additional material requested to have the workpiece in its finished form. This is often defined by a number for each side, such as 3 mm per side for a 6 mm allowance in total. With cut-to-size die blocks, you would incorporate this allowance in your order specifications and make sure to mention it on the order.
Breakdown of Machining Allowance Layers
Total allowance is a stack of four layers, and each one exists for a reason.
| Layer | What it covers | Planning figure per side |
| 1. Surface | Scale, seams, laps and the decarburized skin left by hot working | 1.6% of the dimension, usually not under 2 mm |
| 2. Geometry | Bow, camber, out-of-flat and cutting tolerance | 0.3–0.5 mm |
| 3. Heat treatment | Hardening movement, residual scale or decarburization | 0.15% of the dimension, minimum about 0.3 mm |
| 4. Finishing | EDM recast removal, polishing | Small; set by the finishing process |
Layer 1: surface. Hot rolling and forging leave scale, seams and a skin where carbon has burned out. That soft skin won’t harden properly, so it must go. The AISI benchmark for hot-rolled flats and squares is removal of at least 1.6% of the dimension per side (2.4% for resulfurized steel). It was written for carbon and alloy bars, so treat it as a floor for tool steel. Decarburization depth is measured to ASTM E1077 or ISO 3887.
Layer 2: geometry. No bar is perfectly straight or flat, and long pieces bow more. Cutting adds tolerance, and length is the loosest dimension: +3/+8 mm on Uddeholm’s saw-cut stock, up to +35 mm in some precision flat programmes. Never rely on sawn length for a fit.
Layer 3: heat treatment. The sound workflow is rough machine, stress relieve, semi-finish, harden, grind. Uddeholm recommends 650°C for two hours after roughing H13; Virat’s DB6 guidance is 600–650°C. The Böhler-Uddeholm D2 data sheet sets a minimum of 0.15% per side, but only with stress relief, and Uddeholm’s oil-hardening Arne steel lists 0.25%. Movement can be small: on a 100 × 100 × 25 mm H13 sample, thickness changes 0 to +0.05% after air hardening and up to +0.30% after oil hardening. Scale and decarburization from hardening must also be ground off, so the allowance is never just the movement figure.
Layer 4: finishing. Wire EDM leaves a recast layer. Uddeholm advises removing it by grinding or stoning, then re-tempering about 25°C below the previous tempering temperature. Polishing needs little stock.
Formula and Worked Example
Per side: cleanup (the greater of 2 mm or 1.6% of the dimension) + geometry buffer (0.5 mm) + grinding stock (0.15% of the dimension, minimum 0.3 mm). Order size = finished size + 2 × that total.
For instance, a D2 block, which has a final measurement of 250 × 150 × 50 mm owing to the black flat finish, requires a thickness of 4.9, 3.2 and 2.8 mm on each side. This means that one should order something in the order of 260 × 157 × 56 mm with the understanding that this is merely an estimate rather than a guarantee.
Seven mistakes that cost money
- Writing “+5 mm” without saying per side or total.
- Using one allowance for every grade and condition.
- Ignoring bow on long flats.
- Skipping stress relief between roughing and finishing.
- Accepting a gas-cut block to save a few rupees.
- Expecting ESR to shrink the allowance. ESR cleans the inside of the steel. The surface still carries scale and decarb.
- Hoping allowance will fix internal defects. It won’t. For critical blocks, ask for ultrasonic testing.
What to send with your enquiry
- Grade and drawing, with finished size (L × W × T)
- Process route: use as supplied, or harden after machining
- Heat-treatment method: vacuum or atmosphere furnace
- Supply condition wanted: black, milled or ground
- Cutting method and tolerance (saw cut, plus-only or plus-minus)
- Documents needed: MTC, UT, spectro check
- Quantity and delivery location
Specific Scenarios and Add-Ons
Pre-hardened die blocks (DB6, H13, P20). Virat supplies DB6 annealed or hardened and tempered, typically at 38–44 HRC. If you machine the block as supplied, Layer 3 disappears. Keep Layers 1, 2 and 4, and confirm the condition at order stage.
Hardening after machining (D2, D3, soft H13). Use all four layers. Machine soft, stress relieve, harden, then grind.
Wire EDM. Blocks for eroding are often bought hardened and ground, sometimes with start holes. Allow for recast removal and agree finishing stock with your EDM shop.
Flame or plasma-cut blanks. Avoid them for alloy tool steel. Thermal cutting leaves a hardened heat-affected zone and cracking risk, and needs far more stock. Band-sawing is the safer route.
Large forged blocks. Allowance grows with size, so never reuse a 100 mm figure on a 400 mm block. For heavy die blocks, ask for ultrasonic testing. Virat supplies DB6 die blocks with extra forging reduction and double tempering for better UT quality.
Nitriding. Nitrided cases are shallow (about 0.12–0.20 mm in Uddeholm’s H13 examples), so finish the block first and treat nitriding as a surface step, not an allowance layer.
Add-ons to request on your enquiry:
- Bandsaw cut-to-size and surface machining
- Annealed or hardened-and-tempered supply; ESR or non-ESR
- Ultrasonic testing
- Mill Test Certificate (EN 10204 3.1 where applicable), spectro and hardness reports
- Ground reference faces with squareness and parallelism limits
- Batch-wise traceability
Common Material Grades for Cut-to-Size Die Blocks
Allowance logic changes with the grade and its supply condition:
| Grade (AISI / DIN) | Typical use | Allowance note |
| DB6 / 1.2714 (L6) | Hammer and press forging dies | Often supplied hardened and tempered, so no heat-treatment layer |
| H13 / 1.2344 | Die casting, extrusion, hot forging | Air or vacuum hardening keeps movement small; stress relief still applies |
| H11 / 1.2343 | Forging and aluminium extrusion dies | Plan like H13 |
| D2 (HCHCr) / 1.2379 | Blanking and forming dies, punches | Air hardening; keep at least 0.15% per side with stress relief |
| D3 (HCHCr) / 1.2080 | High-abrasion, long-run tooling | Oil hardening; leave more grinding stock than D2 |
| P20 / 1.2311 | Plastic mould blocks | Usually pre-hardened; no heat-treatment layer |
| P20+Ni / 1.2738 | Large mould blocks | Better through-hardening in thick sections |
Sourcing and Customization Options
Virat Special Steels has nearly 3,500 tons in over 35 grades available at its yards in Ludhiana and Gurugram, resulting in large amounts of cut-to-size die blocks shipped out from stock. The billets originate from mills such as Swiss Steel, NLMK Verona, Lucchini and ThyssenKrupp. Blocks reach you in four conditions, each trading price for convenience:
- Saw-cut black block: lowest cost per kg, most allowance to remove.
- Rough-milled: surface layer gone, flatter.
- Six-side milled: close to size, less machining time. Check the stock left if you will harden.
- Hardened and ground: ready for EDM or fitting, with no allowance for further heat treatment.
Include these on your enquiry:
- Grade and delivery condition
- Finished size and order size, stating per side or overall
- Faces to be ground, with tolerances
- Hardening plan and target hardness
- Testing and certificates needed
- Quantity and delivery date
Contact VIRAT for Drawing-Based Sizing and a Quotation
Let us know your engineering drawing, steel grade, dimensions after machining (L x W x T), desired supply condition, volume, and destination point for supply by Virat Special Steels. Our experts will assist you in estimating machining allowance and provide appropriate die blocks as per your needs.
You may get in touch with us at +91-98140 21775 or write to us at info@viratsteels.com to request for a quotation. We manufacture DB6, H13, H11, D2, D3, and P20 tool and die steels from our Gurugram and Ludhiana plants, supplied across India as per availability.
Frequently Asked Questions
1. How much machining allowance should I leave on a die block? Plan 3–6 mm per side on black stock, 1–2 mm on rough-milled and 0.2–0.4 mm on six-side milled blocks, plus grinding stock if you will harden afterwards.
2. Is machining allowance per side or total? Normally per side. A 3 mm allowance adds 6 mm to each dimension, so always state “per side” or “overall” on your enquiry.
3. How much allowance should I keep for grinding after heat treatment? At least 0.15% of the dimension per side for D2 after stress relief. Oil-hardening grades need more; Uddeholm lists 0.25% for its O1-type Arne steel.
4. Do pre-hardened DB6 (DIN 1.2714) die blocks need heat-treatment allowance? Not if you machine them as supplied, typically 38–44 HRC. Keep the surface, geometry and finishing allowances only.
5. What do black, rough-milled and six-side milled mean? Black keeps the as-forged or as-rolled skin. Rough-milled has the skin removed with stock left. Six-side milled is square and parallel, close to final size, so you can start machining straight away.
6. What do “hot die steel”, “HCHCr”, “OHNS” and “die block” mean? Hot die steel is hot-work steel such as H13, H11 and DB6. HCHCr is high-carbon, high-chromium cold-work steel (D2 and D3). OHNS is oil-hardening non-shrinking steel, usually O1. A die block is a large forged or rolled block used for forging and casting dies.
7. Can I flame-cut or plasma-cut a die block? Avoid it for alloy tool steel. These processes will create a hardened heat-affected area, with the possibility of fracture and wasted material. Instead, consider using a band saw.
8. How much stock should I leave for wire EDM? Enough to remove the recast layer by grinding or stoning, followed by re-tempering about 25°C below the last tempering temperature. Agree exact stock with your EDM shop.
9. What tolerance can I expect on cut length? Length is the loosest dimension. Published saw-cut tolerances run from +3/+8 mm to +35 mm, so ask your supplier for its tolerance and never rely on sawn length for a fit.
10. Db6 or H13 for forging die blocks? The typical material for hammering and press dies is DB6 (DIN 1.2714), while H13 (DIN 1.2344) is the preferred alloy for hot-working conditions like die casting, extrusion, and hot forging. This depends on temperature, impact loads, die configuration, and service life.
11. Does D2 or O1 (OHNS) need more allowance? O1, an oil-hardening grade, needs more grinding stock than air-hardening D2. “Non-shrinking” does not mean no movement.
12. Can I buy a small cut piece instead of a full bar? Yes. Virat Special Steels can provide steel that is cut to size depending on the grade, dimensions and availability of stock. Please inform us of your desired dimensions and quantities.
13. Is cut-to-size priced per kg or per piece? Most manufacturers charge according to the overall weight including the costs of cutting and machining. The extra allowance will be reflected in the weight, too, so you should size it accurately and ask them for your cutting estimate.
14. How can I check I received the grade I ordered? Ensure that the heat number on the material marking is the same as stated in the Mill Test Certificate (MTC). Another way would be to ask for an OES analysis to prove the steel grade. Spark testing cannot be considered a reliable way of verifying the alloy tool steel grade.
15. Can I get MTC and ultrasonic testing on cut-to-size blocks? Yes, request them at order stage. Virat supplies MTC (EN 10204 3.1 where applicable), UT-tested material and spectro verification, subject to grade and product.
16. How fast can I get a quotation and delivery? To receive a quotation from Virat Special Steels, share your steel grade, drawing or size, quantity, and the place where the delivery will take place. The lead time varies from time to time, based on availability of material, any cutting/machining work, testing, and transport.
17. How do I calculate die block weight? Length × width × thickness in mm ÷ 1,000,000 × 7.85 gives kg, using a typical tool steel density of 7.85 g/cm³. A 250 × 150 × 50 mm block weighs about 14.7 kg.
18. Where can I buy cut-to-size die blocks in India? Virat Special Steels supplies DB6, H13, H11, D2, D3 and P20 die blocks from ready stock at Ludhiana and Gurugram, with PAN India delivery, subject to grade and size.
Lucchini DB6 Tool Steel (DIN 1.2714): Complete Guide to Grades, Properties & Applications in India
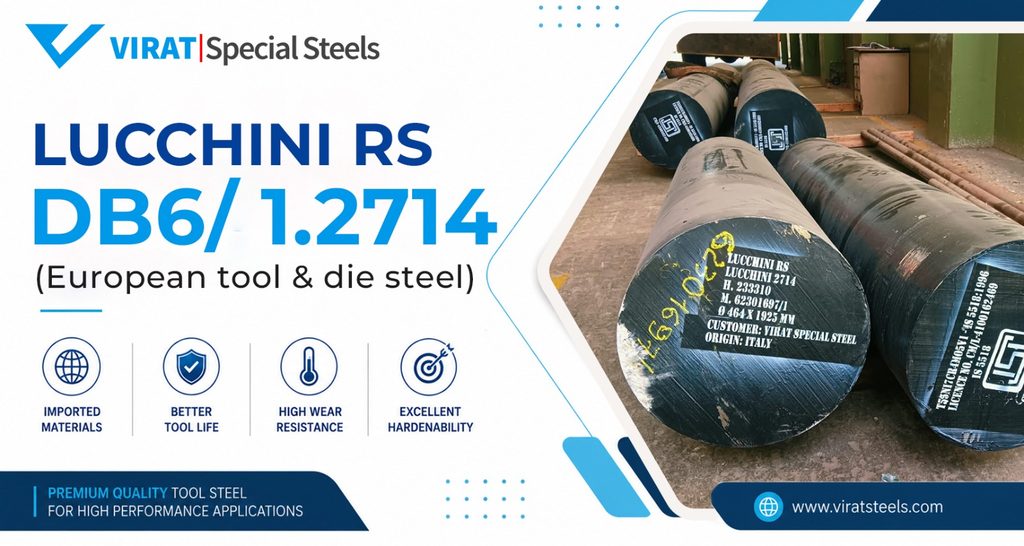
The choice of the appropriate tool steel involves a compromise between hardness, wear resistance, impact toughness, thermal fatigue resistance and the general tool life. While generic steel grades are common, specialized imported tool steels are vital for demanding applications such as hot work, forging and cold stamping.
Lucchini Italy is the international reference for ultra-clean tool steels with high durability. Complete guide on technical properties, international & IS standards, manufacturing processes, detailed grade comparison and procurement of tool steel in India.
What is Lucchini DB6 Tool Steel?
Lucchini DB6 is a low-alloy steel for hot work and impact tools. High Nickel content (1.50″–” 1.80%) formulated and secondary metallurgical refined (EAF->LF->Vacuum Degassing->ESR) This process provides structural purity and minimum non-metallic inclusions with uniform hardenability from core to surface.
Material Standards & Cross-Reference
- DIN / EN Standard: DIN 1.2714 / EN ISO 4957 (56NiCrMoV7)
- AISI Standard: AISI L6 (Modified)
- JIS Standard: SKT4
- IS Standard (India): T55Ni7Cr4Mo5V1 equivalent
Mechanical and Physical Properties
| Property | Value / Specification | Remarks |
| Toughness | Excellent | Resists cracking under heavy shock |
| Impact Resistance | High | Critical for hammer and forging dies |
| Wear Resistance | Good to moderate | Suitable for high-impact hot work |
| Hardenability | Good | Provides consistent through-hardening |
| Dimensional Stability | Good | Maintains shape during thermal cycles |
| Large Section Performance | Excellent | Ideal for heavy forging die blocks |
Same Chemistry on Paper, a Different Story on the Ground
On a certificate, Lucchini DB6 Tool steel and local DB6 tool steels can look almost identical — both fall within the same DIN 1.2714 tool steels chemical window. The real difference shows up upstream of the numbers, in how tightly that chemistry is held, batch after batch, and how clean the steel is once it’s melted and forged.
| Element | Lucchini DB6 / 1.2714 (%) DOCX | Standard Local 1.2714 (%) DOCX | Metallurgical Function DOCX |
| Carbon (C) | 0.50 – 0.60 | 0.50 – 0.60 | Controls baseline hardness and yield strength. |
| Silicon (Si) | 0.10 – 0.40 | 0.10 – 0.40 | Increases oxidation resistance and strength. |
| Manganese (Mn) | 0.60 – 0.95 | 0.60 – 0.95 | Enhances deep hardenability. |
| Chromium (Cr) | 0.80 – 1.20 | 0.80 – 1.20 | Enhances wear resistance and hardenability. |
| Molybdenum (Mo) | 0.35 – 0.55 | 0.35 – 0.55 | Retains high-temperature yield strength. |
| Nickel (Ni) | 1.50 – 1.80 | 1.50 – 1.80 | Primary driver for extreme impact toughness. |
| Vanadium (V) | 0.07 – 0.15 | 0.05 – 0.15 | Refines grain structure and carbide formation. |
| Phosphorus (P) | max 0.015 | max 0.030 | Kept low to prevent cold shortness/brittleness. |
| Sulfur (S) | max 0.010 | max 0.030 | Kept low to preserve steel cleanliness and fatigue life. |
Key takeaway: nominal composition alone doesn’t separate premium DB6 from ordinary DB6 tool steels. What matters far more is the consistency of chemistry control, steel cleanliness, and manufacturing discipline behind that certificate — and that is precisely where an established European mill like Lucchini has a structural advantage over less consistent local supply.
Manufacturing & Heat Treatment Parameters
- Soft Annealing: Heated to 680–720°C, slowly furnace cooled. Delivered (annealed) Hardness: max 229–248 HB (≈ 22–24 HRC)
- Stress Relieving: 600–650°C, following rough machining, then air cooled slowly.
- Hardening (Quenching): Austenitized at 840–870°C, quenched in oil or vacuum pressure gas.
- Double Tempering: Reheated to 540–600°C (minimum 2 cycles) to stabilize dimensions and relieve retained austenite.
Recommended Working Hardness by Application
| Application | Target Hardness |
| Drop Hammer Dies & Heavy Impact Tooling | 38 – 42 HRC |
| Press Forging Dies & Inserts | 44 – 48 HRC |
| Hot Shear Blades & Trimming Tools | 48 – 52 HRC |
NOTE: Lower hardness (38-42 HRC) is more shock and impact resistant; higher hardness (48-52 HRC) is more wear resistant and holds a sharper edge. Choose based on whether you experience more impact load or more abrasive wear in your tooling.
Comparison Table: Lucchini DB6 Tool Steel vs. Local Indian DB6 Tool Steel
| Parameter / Feature | Lucchini Italy DB6 Steel (DIN 1.2714) | Local Indian DB6 Tool Steel | Practical / Industrial Impact |
| Manufacturing & Melting Route | Electric Arc Furnace (EAF) + Ladle Furnace (LF) + Vacuum Degassing (VD) / ESR option | Standard EAF or Induction Furnace melting | Superior steel cleanliness, lower gas content, and higher purity in Lucchini steel. |
| Forging Reduction Ratio | Multi-directional 3D forging (Min. 4:1 upsetting ratio) | Standard 2D forging or conventional rolling | Higher structural integrity and better grain flow alignment. |
| Microstructural Uniformity | Extremely high and consistent throughout the block | May vary across core to surface | Predictable machining, heat treatment, and die performance. |
| Purity & Inclusion Levels | Strictly controlled Sulfur (≤ 0.030%) & Phosphorus (≤ 0.030%) | Controlled to basic standards (0.035%) | Lower inclusion levels directly improve fatigue life and crack resistance. |
| Impact Toughness | Outstanding and uniform (20–25 J/cm²) | Moderate to high (can vary by batch) | Higher crack resistance under extreme hammer shock loads. |
| Through-Hardening (Large Blocks) | Uniform hardness even in large sections (400 mm) | Depends on forging quality and section size | Prevents soft core issues in massive die blocks. |
| Heat Treatment Response | Highly predictable and repeatable across batches | May vary slightly between batches | Minimal distortion risk and consistent target HRC achievement. |
| Thermal Fatigue Resistance | Superior resistance to heat checking | Application dependent | Withstands repeated heating/cooling cycles longer during hot forging. |
| Impact Toughness | Up to 30% – 40% increase in production cycles | Baseline standard die life | Significantly reduces shop floor downtime and tooling replacement costs. |
| Quality Documentation | 100% EN 10204 3.1 MTC with SEP 1921 Class D/d UT certification | Standard MTC and basic UT reporting | Complete global batch traceability and defect-free guarantee. |
| Initial Material Cost | Premium / Higher investment | Cost-effective / Lower initial price | Higher initial cost of Lucchini steel is offset by lower tooling cost-per-component. |
Key Advantages of Lucchini DB6 tool steel (DIN 1.2714)
- Extreme Impact Toughness: High nickel (1.50–1.80%) prevents cracking under heavy drop-hammer shock loading.
- In demanding forging applications, premium-quality DB6 with controlled metallurgy, cleanliness and appropriate heat treatment can help improve die reliability and service life compared with lower-quality material.
- Deep Through-Hardening: Delivers uniform core-to-surface hardness in large blocks (400 mm).
- Thermal Fatigue Resistance: Withstands heat checking from repeated heating and cooling cycles.
- High Metallurgical Cleanliness: Low sulfur and phosphorus reduce inclusions and enhance fatigue strength.
- Perfect Quality Assurance: Certified by 100% Ultrasonic Testing (UT) and EN 10204 3.1 Mill Test Certificates. Available Sizes of DB6 Tool Steel
Virat Special Steels supplies Lucchini DB6 Tool Steel in a wide range of standard and custom sizes to meet the requirements of die makers, tool rooms, automotive, engineering, and precision manufacturing industries.
Custom Processing Services
To minimize machining time and material wastage, we also offer:
- Precision cut-to-size material
- Bandsaw cutting
- Surface machining (on request)
- Bulk supply with batch-wise traceability
- Material Test Certificate (MTC) and EN 10204 3.1 certification (where applicable)
Case Study: DB6 Increases Die Life by 40%
Customer Challenge
A drop-forging plant for automotive components experienced premature die cracking of crankshaft forging dies made from standard hot work steels leading to expensive downtime.
Solution
The tooling was upgraded to DB6 (DIN 1.2714) supplied by Virat Special Steels, vacuum heat treated and double tempered to an optimized 46-48 HRC.
Results
40% increased die service life Eliminate catastrophic die cracking in high energy impact Lower maintenance and machine downtime Forged at a lower cost per part
Certifications Available
Reputable suppliers typically provide:
- Mill Test Certificate (MTC)
- Ultrasonic Tested Material
- Hardness Test Report
- Chemical Test Report
Buyer’s Guide: Selecting the Appropriate DB6 Tool Steel
Some important points to consider before buying DB6 Tool Steel (DIN 1.2714) to get the best out of your application:
1. Choose the Right Hardness
Pick the hardness for your application:
- 38-42 HRC – Greater toughness and impact resistance
- 50-56 HRC – Increased wear resistance and extended tool life
2. Choose the required form of material
DB6 Tool Steel is supplied in:
- Forged and Rolled blocks
- Round and Flat Bars
- ESR and Non ESR Blocks
3. Material Quality Inspection
Always ask for:
- Mill Test Certificate (MTC) Ultrasonic Tested Material
- Material Traceability Spectro Tested Material
4. Match the App
Select DB6, depending on your tooling needs, such as:
- Forging Dies
- Hammer Dies
- Extrusion
- Holders for
- Casting Dies
5. Select a Trusted Supplier
Join hands with a supplier who can support with ready stock, custom machining, technical support and PAN India delivery for consistent quality and timely supply.
Why Choose Virat Special Steels for Lucchini DB6?
Virat Special Steels is a trusted supplier of imported tool steels to forging, die-making, automotive, engineering and manufacturing industries across India. With over 70 years of experience in special and tool steels, we provide quality-assured material, trusted sourcing, technical support and application-driven solutions.
Imported Lucchini DB6 Tool Steel We supply Lucchini DB6 Tool Steel (DIN 1.2714) for applications where high toughness, impact resistance, hardenability, and reliable tooling performance are required, with relevant mill documentation and material traceability subject to the specific product and supply condition.
Ready Stock Availability Our ready-stock inventory helps customers reduce procurement lead times and maintain production schedules. DB6 material can be supplied in different forms and sizes depending on availability and project requirements.
DB6 Round Bars & Flat Bars We supply DB6 round bars and flat bars in standard and customized dimensions — diameter, thickness, width, and length — subject to stock availability.
Forged DB6 Blocks For heavy-duty tooling and die applications, we offer forged DB6 blocks in suitable dimensions for machining large dies, die inserts, and other industrial tooling components.
Cut-to-Size Services DB6 Tool Steel can be supplied in cut-to-size dimensions according to customer requirements, helping reduce material wastage and bring material closer to final machining dimensions.
Machining Services Where required, we provide machining and material preparation services for DB6 Tool Steel, reducing in-house preparation time before the material moves to further tooling operations.
UT-Tested Material For applications where internal material quality is critical, Ultrasonic Testing (UT) can be provided according to applicable inspection requirements, helping identify internal discontinuities and support quality verification.
Mill Test Certificate (MTC) DB6 Tool Steel can be supplied with a Mill Test Certificate where applicable, covering heat/lot identification, chemical composition, mechanical properties, and other specified inspection results.
Spectro & Chemical Verification Spectro/chemical verification can be carried out where applicable to support material identification and chemistry verification — customers can discuss specific testing and certification requirements with our technical team before ordering.
PAN India Delivery Our logistics network supports PAN India delivery for forging companies, die makers, tool rooms, automotive manufacturers, engineering companies, and other industrial users.
Technical Support Choosing the right DB6 material involves more than selecting a grade. Our technical team can assist with grade selection, material form, dimensions, hardness requirements, heat-treatment considerations, testing requirements, and application suitability.
Whether you require Lucchini DB6 round bars, flat bars, forged blocks, cut-to-size material, or machined components, Virat Special Steels can help you source the appropriate material for your application.
Our Supply Network Across India
Virat Steels is one of the leading suppliers of DB6 Tool Steel (DIN 1.2714) to the manufacturers in the major industrial hubs of India like Ahmedabad, Rajkot, Pune, Nashik, Aurangabad, Kolhapur, Belgaum, Chennai, Coimbatore, Hosur,Bengaluru, Hyderabad, Faridabad, Manesar, Bhiwadi, Gurugram, Delhi NCR, Ludhiana, Chandigarh, Haryana, Punjab and Jamshedpur.
Our strong logistics network, ready stock and technical knowledge enable us to provide fast PAN India delivery to forging companies, die makers, tool rooms, plastic mould manufacturers, die casting industries and heavy engineering businesses.
Conclusion
The right tool steel choice directly affects the tooling cost per component, production downtime, and product quality. For low volume applications standard die steels may be sufficient but major advantages are available for high duty forging and hammer die work with certified imported grades such as Lucchini DB6 (DIN 1.2714).
An experienced stockiest like Virat Special Steels offers manufacturers across India the facility of genuine imported DB6, ready stock, cut-to-size material and complete metallurgical documentation.
Need DB6 tool steel for your next project? Contact our technical team for availability, required sizes, testing documentation, and quotations.
Get a Quote for Lucchini DB6 Tool Steel
Looking for Lucchini DB6 Tool Steel (DIN 1.2714) or other hot work tool steel in India? Virat Special Steels supplies imported DB6 in round bars, flat bars, forged blocks, rolled blocks, and cut-to-size material, subject to stock availability.
We can also support your requirements with ready stock, MTC, UT-tested material, spectro/chemical verification where applicable, custom machining, and PAN India delivery. Our technical team can assist with material selection, dimensions, hardness requirements, testing documentation, and application-specific requirements.
For other hot work tool steel, cold work tool steels, plastic mould steels, Alloy steel, high speed steel requirements
Call: +91-98140 21775
Email: info@viratsteels.com
Locations: Gurgaon (Haryana) | Ludhiana (Punjab)
Frequently Asked Questions
1. What is Lucchini Tool Steel?
Lucchini tool steel refers to specialized high-cleanliness alloy steels manufactured by Lucchini Italy for forging, die casting, and industrial tooling.
2. Is DB6 a hot work or cold work steel?
DB6 (DIN 1.2714) is classified as a low-alloy hot work tool steel valued for extreme impact toughness.
3. What is the AISI equivalent of DB6 steel?
The closest approximate AISI equivalent is AISI L6.
4. What is the standard hardness of annealed DB6?
In soft annealed condition, DB6 has a maximum hardness of 250 HB (25 HRC).
5. Can DB6 steel be pre-hardened?
Yes, DB6 is frequently supplied in a pre-hardened state (360-430 / 38-44 HRC).
6. Why is Nickel (Ni) added to DB6 tool steel?
Nickel (1.50-1.80) provides deep hardenability and structural impact toughness.
7. What is the quenching medium for DIN 1.2714?
It is typically quenched in oil or vacuum pressure gas after austenitizing at (840-870)
8. Why is double tempering necessary?
Double tempering ensures full transformation of retained austenite and stabilizes dimensional accuracy.
9. How does Ultrasonic Testing (UT) protect buyers?
UT inspection ensures blocks are 100% free of internal voids, pipe shrinkage, or sub-surface cracks.
10. Is DB6 suitable for plastic injection moulds?
Yes, pre-hardened DB6 is widely used for large plastic mould frames requiring core toughness.
11. What is the density of DIN 1.2714 tool steel?
The density is 7.85 g/cm³ (7,850 kg/m³).
12. What is the IS Standard equivalent for 1.2714 steel?
It corresponds to Indian Standard classifications such as T55Ni7Cr4Mo5V1.
13. Why choose Lucchini DB6 over standard local die blocks?
Lucchini DB6 provides superior structural cleanliness, higher impact toughness, and up to 30–40% longer die life.
14.What is stress relieving and when is it done?
Stress relieving involves heating machined tooling to 600–650°C to release internal machining stresses before hardening.
15. What industry sectors heavily consume Lucchini DB6?
Automotive forging, drop-forging plants, aluminum extrusion, and heavy machinery tooling.
16. How can I get authentic Lucchini tool steel in India?
Contact technical stockists like Virat Special Steels, who supply genuine certified imported tool steels with complete MTC documentation.
17. What is the density of DB6 (DIN 1.2714) tool steel?
The density is 7.85 g/cm³ (7,850 kg/m³).
18.Can DB6 steel be supplied pre-hardened?
Yes, DB6 can be supplied pre-hardened, typically in the 38–42 HRC range depending on the intended application.
19. How can I source genuine Lucchini DB6 tool steel in India?
Work with a technical stockist like Virat Special Steels, which supplies certified imported DB6 with complete MTC documentation and batch traceability.